Stay updated with the latest company news, product innovations, exhibition highlights, and industry trends. Explore valuable insights into pressure vessel technologies and global markets.
The difference between 304 and 316L is 2–3 % molybdenum and a carbon limit of 0.03 % instead of 0.08 %. Molybdenum gives pitting resistance; low carbon gives weld corrosion resistance.
Quantified by PREN (Pitting Resistance Equivalent Number = %Cr + 3.3 × %Mo + 16 × %N): 304 ≈ 18–19, 316/316L ≈ 24–26. Higher PREN means greater resistance to chloride‑induced pitting.
Chloride is the enemy, and temperature makes it worse. Austenitic stainless steels are vulnerable to chloride stress corrosion cracking (Cl‑SCC) above roughly 50–60 °C when chlorides are present. AI coolant loops typically run 18–45 °C, which is close enough to matter, not far enough to relax.
316L is the default recommendation for technology cooling system reservoirs and vessels in contact with inhibited glycol, and it is essential at coastal sites, seawater‑cooled plants, or wherever make‑up water chlorides may exceed roughly 100 ppm.
304 is acceptable where water chemistry is tightly controlled, chlorides are reliably low, the loop is fully closed, and the fluid is DI‑treated with a maintained inhibitor package.
Cost: 316L material typically runs 20–40 % above 304 (indicative — varies with nickel and molybdenum spot prices). On a reservoir, that difference is a small fraction of the cost of the GPU equipment the loop protects.
The "L" grade matters for welded tanks. Standard 304 and 316 can sensitize in the heat‑affected zone of a weld, precipitating chromium carbides at grain boundaries and creating intergranular corrosion paths. 304L and 316L are formulated to prevent this.
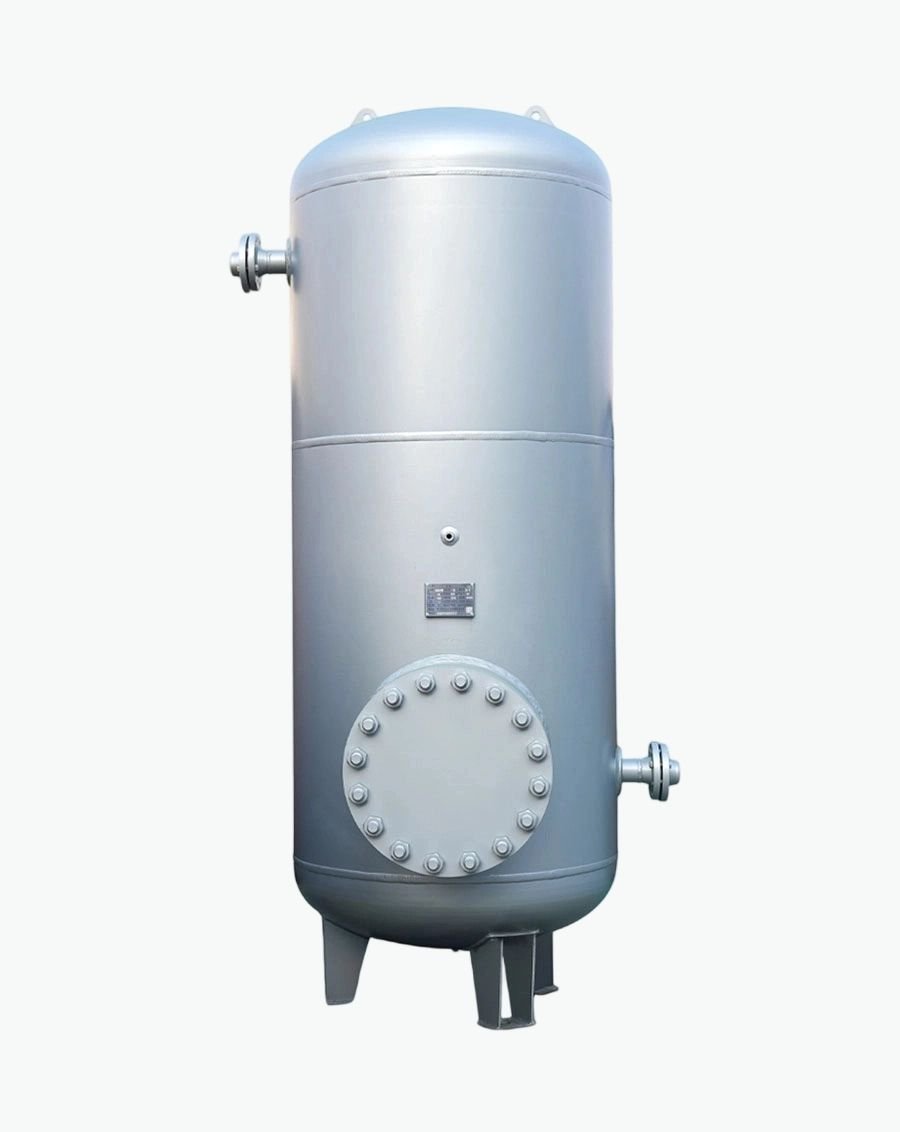
A coolant reservoir in an AI data center technology cooling system is not a passive container. It holds a warm, slightly alkaline, chemically inhibited glycol‑water solution in continuous contact with dissimilar metals — copper cold plates, stainless manifolds, elastomer seals, and on the facility side possibly carbon steel and aluminium — for a design life measured in a decade or more, with no opportunity to inspect or replace it without shutting down a training cluster.
Material failure in this service is not dramatic. It is progressive: pitting initiates at a chloride concentration site, propagates under a deposit, perforates the wall over years, and announces itself as a slow leak detected by a level switch. By then the coolant has been contaminated with corrosion products for a long time, and the cold plates downstream have been accumulating magnetite.
Choosing between 304 and 316L is therefore a decision about chloride exposure, temperature, and water chemistry control — and those three factors are knowable at design stage.
表格
| Grade | Chromium | Nickel | Molybdenum | Carbon (max) | Manganese | Silicon |
|---|---|---|---|---|---|---|
| 304 | 18–20 % | 8–10.5 % | — | 0.08 % | ≤ 2 % | ≤ 0.75 % |
| 304L | 18–20 % | 8–12 % | — | 0.03 % | ≤ 2 % | ≤ 0.75 % |
| 316 | 16–18 % | 10–14 % | 2–3 % | 0.08 % | ≤ 2 % | ≤ 0.75 % |
| 316L | 16–18 % | 10–14 % | 2–3 % | 0.03 % | ≤ 2 % | ≤ 0.75 % |
Both are austenitic (300‑series) chromium‑nickel stainless steels. Both rely on a self‑repairing passive chromium oxide (Cr₂O₃) film only nanometres thick, which forms spontaneously in the presence of oxygen and is what makes them "stainless". Both are non‑magnetic in the annealed condition.
The two differences that matter:
Molybdenum (2‑3 % in 316, zero in 304). Molybdenum stabilizes the passive film specifically against chloride attack. Chloride ions are small, aggressive and mobile; they locally break down the oxide film and initiate pitting. Molybdenum raises the chloride concentration and the temperature at which that breakdown occurs. This is the entire reason 316 exists as a separate grade.
Carbon (0.03 % max in the L grades, 0.08 % max in the standard grades). When austenitic stainless steel is held in the roughly 450‑850 °C range — which happens inevitably in the heat‑affected zone beside any weld — carbon combines with chromium to precipitate chromium carbides at grain boundaries. The chromium is drawn out of the adjacent metal, leaving a chromium‑depleted zone that no longer passivates. This is sensitization, and it produces intergranular corrosion and weld decay: the metal loses its corrosion resistance precisely along the welds, which are also the places with the highest residual stress and the most complex geometry. The "L" (low‑carbon) grades have too little carbon to form significant carbides, so they can be welded without post‑weld heat treatment.
For a fabricated tank with dozens of metres of weld, this is not an optional refinement. Specify 304L or 316L, not 304 or 316.
\(PREN = \%Cr + 3.3 × \%Mo + 16 × \%N\)
| Grade | PREN |
| 304 / 304L | ≈ 18‑19 |
| 316 / 316L | ≈ 24‑26 |
| Duplex 2205 (for reference) | ≈ 34‑38 |
| Super‑austenitic 904L (for reference) | ≈ 34‑36 |
PREN is an empirical index, not a guarantee, and it should be used to compare grades rather than to predict service life. But the gap between 19 and 25 is significant and consistent: as a rough engineering rule, higher PREN grades tolerate proportionally higher chloride concentrations and higher temperatures before pitting initiates. Molybdenum's weight of 3.3 in the formula means the 2‑3 % Mo in 316 contributes around 7‑10 PREN points on its own — the largest single difference between the two grades.
CPT is the temperature above which pitting initiates in a given chloride environment, commonly measured per ASTM G48. It is a function of both grade and chloride concentration, so a single number is meaningless without specifying the environment. What can be said with confidence:
At any given chloride concentration, 316L's CPT is substantially higher than 304's — commonly by 15‑25 °C in standardized test media.
Both grades' CPT falls sharply as chloride concentration rises. A 304 component that is entirely comfortable in 20 ppm chloride water can pit within months in 200 ppm chloride water at 40 °C.
Laboratory CPT values are measured in aggressive, well‑defined media and do not transfer directly to service conditions. Use them to rank grades, not to set operating limits.
The honest engineering statement: for AI coolant service at 18‑45 °C, both grades are viable if chlorides are kept genuinely low; 316L is required as chloride rises or as confidence in water chemistry control falls.
This is the failure mode that concerns corrosion engineers most in warm aqueous service, because it is sudden, brittle and catastrophic rather than gradual.
The three conditions that must all be present:
Tensile stress — residual stress from welding and forming is usually sufficient; no applied load needed
Chloride ions — commonly cited thresholds start around 50‑200 ppm, and lower in the presence of crevices or deposits where chlorides concentrate
Temperature above roughly 50‑60 °C
Both 304 and 316 are susceptible. Molybdenum improves resistance somewhat but does not eliminate it — 316 is not considered Cl‑SCC‑resistant in the way duplex or ferritic grades are. Where the combination is genuinely unavoidable, the answer is a duplex grade, a nickel alloy, or removing the chloride.
The AI cooling relevance: technology coolant systems commonly run 18‑32 °C supply for current‑generation hardware, with returns higher. That is below the classic Cl‑SCC threshold — but the threshold is not sharp, it drops in crevices and under deposits where chlorides concentrate by evaporation, and next‑generation platforms are moving toward warmer coolant (up to 45 °C inlet is referenced for future NVIDIA generations under the ASHRAE W45 class). A tank specified today for a 32 °C loop may serve a 45 °C loop in five years. Design for the warmer case.
A practical chloride ceiling for grade selection: keeping chloride below ~100 ppm at temperatures up to ~40 °C is a commonly used basis for accepting 304; above that, or above ~45 °C, move to 316L. Treat these as planning values to be confirmed against your specific water supply analysis and coolant supplier's guidance — not as absolute limits.
The galvanic series in a cooling loop typically runs, from most noble (cathodic) to most active (anodic): Graphite / platinum → copper → stainless steel (passive) → tin → lead → aluminium → carbon steel → zinc
The practical consequences for an AI loop:
Copper cold plates + stainless manifolds and tank: a modest couple. Stainless is passive and reasonably noble, so the driving force is limited — provided the stainless stays passive. If it pits or if the passive film breaks down, the local behaviour changes.
Aluminium anywhere in the circuit + copper: a serious couple. Potential differences on the order of 0.5‑0.7 V in an aqueous electrolyte are commonly cited, and aluminium will corrode preferentially at a greatly accelerated rate without an effective inhibitor package or dielectric isolation.
Carbon steel + stainless: carbon steel becomes the anode and corrodes, generating magnetite that circulates to the cold plates.
Inhibitor packages work by forming protective films on each metal independently — azoles (tolyltriazole, benzotriazole) for copper, silicates or phosphonates for aluminium and steel. This is "layered inhibition", and it is why the coolant must be matched to the actual metals present, not chosen generically.
Two specification actions follow:
Keep the reservoir stainless and keep aluminium out of the technology cooling system. This minimizes the number of active couples in the clean loop.
Use dielectric isolation (insulating gaskets, non‑conductive unions) at any dissimilar‑metal joints.
Specifying 316L and receiving a poorly fabricated 316L tank is a common outcome. The fabrication details matter as much as the grade.
TIG (GTAW) with inert gas back purge on the root pass. Without back purge, the underside of the weld oxidizes, forms a heat‑tint layer, and becomes chromium‑depleted — a corrosion initiation site that is invisible from the outside. Ask for the welding procedure specification and confirm back purging is required. Any weld discoloration (blue, purple, straw) is an oxide layer with depleted chromium beneath it. It must be removed mechanically or chemically. A properly finished weld is silvery and matches the parent metal.
Passivation. After fabrication and weld cleaning, the surface should be passivated — typically by nitric or citric acid treatment — to remove free iron contamination (from steel tooling, grinding media, or transport) and to restore a uniform, thick chromium oxide film. Free iron on a stainless surface rusts, and rusting iron particles in a coolant loop are exactly what you specified stainless steel to avoid.
Electropolishing. Optional but valuable where cleanliness is critical. Electropolishing preferentially dissolves the surface peaks, producing a microscopically smooth, bright surface with improved passivity and reduced sites for biofilm adhesion and particulate retention.
Surface finish. Specify the internal surface roughness, expressed as Ra. Common targets are Ra ≤0.8 μm for general clean service and Ra ≤0.4 μm where pharmaceutical‑ or food‑grade cleanability is required. A rough internal surface retains particulate, shelters microorganisms and initiates pitting.
Design details that prevent corrosion:
No crevices. Crevices are where chlorides concentrate and where oxygen is depleted, creating the differential‑aeration cells that drive crevice corrosion — which initiates at lower chloride levels than pitting. Design out dead legs, use full‑penetration butt welds rather than lap joints, and avoid unsealed crevices at flanges and supports.
Full drainage. A tank that cannot fully drain retains a concentrated residue that attacks the metal during shutdown.
No contact with carbon steel. Separate storage, separate tooling, separate lifting equipment. Iron contamination is the most common cause of "stainless steel rusting".
Proper support design to avoid stress concentration and fretting at contact points.
Relevant standards: ASTM A240 (stainless plate, sheet and strip for pressure vessels), ASTM A277 (stainless bar), ASME BPVC Section VIII Div. 1 (pressure vessel construction), EN 10088 (stainless steel compositions and technical delivery conditions), EN 13445 (unfired pressure vessels), and PED 2014/68/EU for EU conformity.
Specify 316L when any of the following is true:
The site is coastal or draws make‑up water with elevated chlorides
The plant uses seawater or brackish‑water cooling, or a cooling tower with high cycles of concentration
Specializing in pressure vessel manufacturing, we provide reliable, certified, and customized solutions for customers across diverse industries worldwide.
No.268 Xinda Road, High-tech Industrial Park, Longkou City,Shandong Province
Copyright © 2026 Yantai Xinglong Pressure Vessel Manufacturing Co., Ltd All Rights Reserved.


 عربي
 Español
 Русский
