Stay updated with the latest company news, product innovations, exhibition highlights, and industry trends. Explore valuable insights into pressure vessel technologies and global markets.
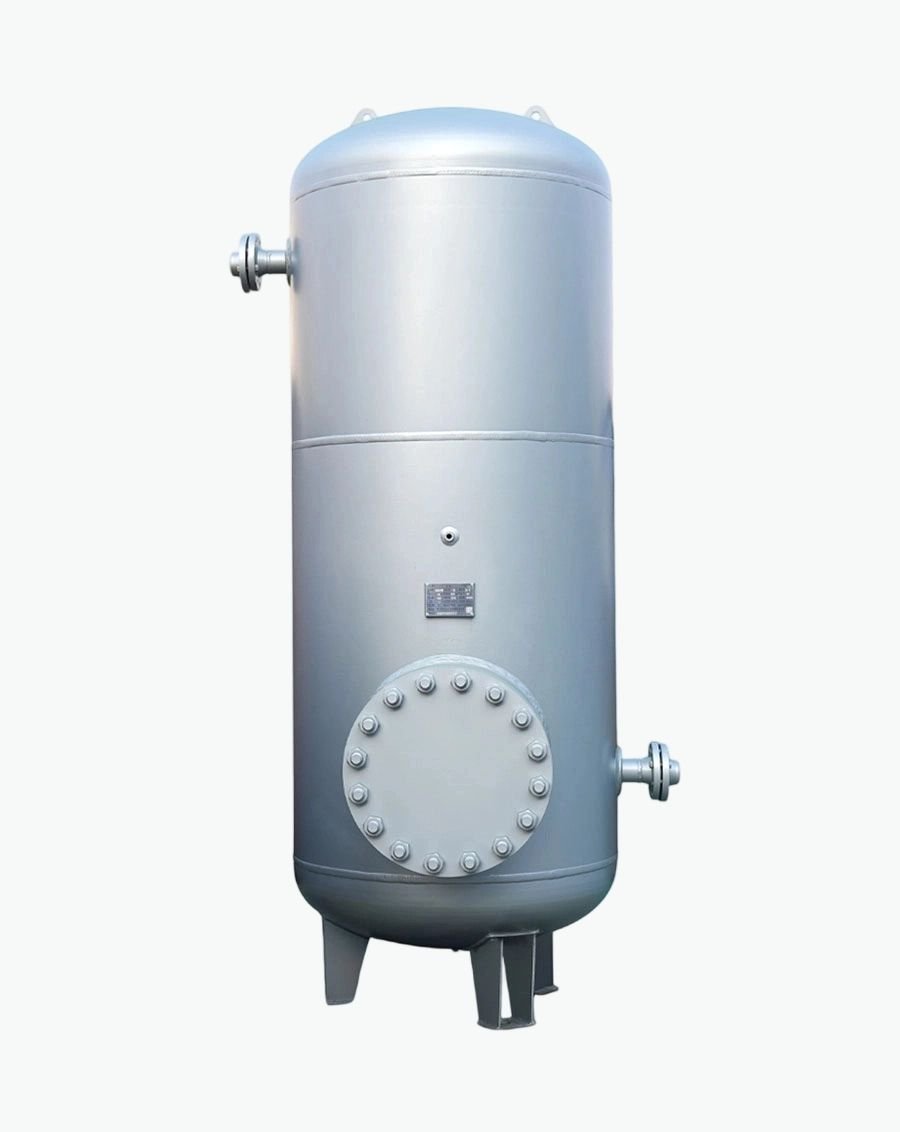
Air receiver tank requirements vary dramatically across industrial sectors reflecting diverse operational conditions, regulatory frameworks, quality standards, and performance expectations. While fundamental pressure containment principles remain constant, application-specific demands drive material selections, design configurations, certification requirements, and maintenance protocols that differ substantially between manufacturing facilities, healthcare institutions, food processing plants, and other specialized environments.
Generic one-size-fits-all approaches prove inadequate serving these varied needs potentially resulting in underspecified equipment failing to meet critical requirements or over-engineered solutions imposing unnecessary costs. Optimal air receiver selection requires deep understanding of sector-specific challenges including contamination sensitivities, hygiene mandates, uptime criticality, space constraints, and compliance obligations unique to each industry vertical.
This comprehensive guide examines air receiver tank selection criteria across major industrial segments providing detailed recommendations tailored to distinct operational profiles. By understanding how manufacturing, healthcare, food and beverage, pharmaceutical, electronics, and other sectors approach compressed air storage differently, procurement specialists, engineering teams, and facility managers can specify equipment delivering appropriate performance levels without excessive investment or inadequate protection.
General manufacturing encompassing metal fabrication, automotive assembly, woodworking, textiles, and packaging represents largest air receiver market segment accounting for 40-45% of total volume. Characteristics include:
Operating Conditions: Moderate pressure requirements (7-10 bar), intermittent demand patterns with significant peak-to-average ratios, mixed indoor/outdoor installations, and variable environmental exposures depending on facility type. Corrosion risks range from mild (climate-controlled assembly plants) to severe (coastal shipyards, chemical-exposed metal finishing shops).
Material Preferences: Carbon steel dominates 70-80% of installations due to cost-effectiveness and adequate performance for general service. Epoxy internal coatings extend service life preventing rust contamination though not strictly required for non-critical applications. External coating systems protect against atmospheric corrosion with specifications varying by location severity.
Stainless steel adoption increases in higher-value manufacturing (precision machining, aerospace components) where air quality affects product integrity. Price premiums justified through reduced maintenance and elimination of rust-related quality issues.
Sizing Considerations: Large volume receivers (2000-10000+ liters) centralize storage serving multiple production lines enabling compressor optimization. Smaller point-of-use receivers (100-500 liters) supplement main storage near high-demand equipment smoothing transient spikes. Total system storage typically targets 10-15 liters per m³/min compressor capacity balancing energy efficiency against capital costs.
Key Selection Criteria:
● Cost-effectiveness prioritized given large quantities deployed
● Durability supporting 15-20 year service lives with proper maintenance
● Flexibility accommodating production changes and capacity expansions
● Ease of maintenance minimizing skilled labor requirements
● Compatibility with existing distribution infrastructure
Common Pitfalls: Undersizing receivers forcing compressor short-cycling, neglecting condensate drainage leading to internal corrosion, installing inadequate safety relief valves, and failing to plan for future capacity growth requiring premature replacement.
Mining operations, steel mills, cement plants, and heavy manufacturing present extreme service conditions demanding robust equipment:
Environmental Challenges: Abrasive dust infiltration, wide temperature swings (-30°C to +50°C), high humidity underground, corrosive chemical exposures, and physical impact risks from mobile equipment collisions. Standard industrial receivers deteriorate rapidly requiring enhanced protection.
Material Specifications: Heavy-wall carbon steel (12-20mm thickness) withstands mechanical abuse while resisting abrasion. Duplex stainless steel serves coastal mining operations combating salt spray corrosion. Internal epoxy linings rated for immersion service prevent aggressive condensate attack from contaminated air containing particulate matter.
External coatings incorporate abrasion-resistant formulations with ceramic or carbide additives extending surface life. Impact protection cages or barriers shield receivers from vehicle strikes in open-pit operations.
Design Features: Elevated mounting prevents flood damage during heavy rains. Drain systems accommodate high solids loading from dusty environments with larger diameter piping preventing blockages. Redundant safety relief valves ensure protection even if primary valves foul from contamination.
Seismic bracing addresses earthquake risks in mining regions. Foundation designs account for dynamic loads from nearby blasting operations. Lightning protection grounds prevent electrical damage in exposed locations.
Maintenance Adaptations: Extended inspection intervals prove impractical given accelerated degradation necessitating quarterly rather than annual examinations. Remote monitoring reduces personnel exposure to hazardous environments. Modular designs enable rapid replacement minimizing production disruptions.
Spare receiver availability proves critical as delivery lead times to remote sites extend months. On-site storage of critical components (drain valves, gauges, relief valves) enables emergency repairs avoiding extended downtime.
Automotive assembly plants utilize compressed air extensively for pneumatic tools, robotic actuators, paint spraying, and testing equipment creating unique requirements:
Quality Sensitivities: Paint booth applications demand ISO 8573 Class 1-2 air quality requiring oil-free compression and extensive filtration. Receiver tanks must not introduce contamination through internal corrosion or coating degradation. Stainless steel construction eliminates rust particle generation protecting finish quality.
Welding and riveting operations generate vibration transmitting through structural connections requiring flexible piping arrangements preventing fatigue failures. Receivers mounted on isolated pads dampen vibration extending equipment life.
Demand Patterns: Highly cyclical with intense bursts during shift changes, model transitions, and quality testing phases followed by lower steady-state consumption. Large receivers (5000-20000 liters) buffer these fluctuations enabling right-sized compressor installations rather than peak-capacity oversizing.
Just-in-time production philosophies minimize inventory buffers making compressed air reliability critical. Unplanned outages halt entire assembly lines costing $10,000-50,000 per hour in lost production. Redundant receiver banks provide backup capacity during maintenance.
Integration Requirements: Building automation system connectivity enables energy monitoring and predictive maintenance. Smart receivers with IoT sensors feed data to centralized dashboards tracking performance trends. Automated drain systems integrate with facility condensate treatment preventing environmental violations.
Space constraints in dense plant layouts favor vertical receivers maximizing floor space utilization. Aesthetic considerations sometimes apply for visible installations in customer tour areas requiring clean appearance and noise attenuation.
Regulatory Compliance: ASME or PED certification mandatory depending on location. Local fire codes may restrict receiver locations relative to ignition sources. Occupational safety regulations mandate guarding, labeling, and access controls preventing unauthorized interactions.
Healthcare facilities operate critical medical air systems supplying surgical suites, intensive care units, respiratory therapy, and laboratory applications where air quality directly impacts patient safety:
Regulatory Framework: NFPA 99 (US), HTM 02-01 (UK), and similar international standards govern medical gas systems including compressed air. Requirements exceed industrial specifications dramatically:
● Oil-free compressors mandatory eliminating lubricant contamination risks
● Dew point specifications of -40°C or below preventing condensation in distribution piping
● Particulate filtration to 0.01 micron removing bacteria and contaminants
● Continuous monitoring with alarms alerting staff to quality deviations
● Redundant systems ensuring uninterrupted supply during maintenance or failures
Receiver tanks form integral components requiring equally stringent specifications.
Material Mandates: Stainless steel Type 316L construction universally specified eliminating any possibility of rust contamination. Internal surfaces electropolished to Ra < 0.4 μm achieving sanitary finish preventing bacterial adhesion and facilitating cleaning validation.
Welded connections replace threaded fittings eliminating crevices harboring contaminants. Orbital welding procedures ensure smooth internal profiles maintaining flow characteristics. All welds undergo 100% radiographic examination verifying complete penetration and absence of defects.
Certification documentation including material traceability, weld maps, NDE reports, and pressure test records supports regulatory audits and accreditation reviews. Digital archives enable instant retrieval during inspections.
Design Configurations: Dual receiver banks provide redundancy allowing one bank isolation for maintenance while other continues service. Automatic switchover valves maintain uninterrupted supply during transitions. Each bank sized for full facility load ensuring adequate capacity even with half system offline.
Pressure ratings typically 10-12 bar exceeding distribution requirements providing margin for filter pressure drops and future expansion. Safety relief valves set conservatively preventing overpressure while avoiding nuisance trips disrupting critical care.
Location within dedicated medical gas rooms separates from general facility compressors preventing cross-contamination. Positive pressure ventilation maintains clean environment. Access restricted to authorized personnel preventing accidental interference.
Validation and Testing: Initial commissioning includes comprehensive validation protocol:
● Particle counting verifying filtration effectiveness
● Microbiological sampling confirming sterility
● Dew point measurements across operating ranges
● Pressure decay tests identifying leaks
● Alarm function verification ensuring notification reliability
Annual revalidation maintains compliance documenting continued performance. Trend analysis tracks gradual degradation enabling proactive interventions before violations occur.
Maintenance Protocols: Specialized technicians trained in medical gas systems perform all maintenance activities. Lockout/tagout procedures prevent accidental shutdowns affecting patient care. Spare parts inventory ensures rapid repairs minimizing outage durations.
Documentation rigor exceeds industrial norms with every intervention recorded including technician credentials, procedures followed, test results, and supervisory approvals. Regulatory agencies review these records during facility inspections.
Smaller healthcare settings including dental offices, veterinary clinics, and outpatient surgery centers operate scaled-down medical air systems with modified but still stringent requirements:
Scale Considerations: Single compressor serving 2-10 workstations contrasts with hospital central plants. Receiver sizes range 100-500 liters adequate for limited demand though quality standards remain uncompromising.
Space constraints in urban practices favor compact vertical receivers fitting within utility closets.
Noise attenuation proves critical in patient-care adjacent locations requiring soundproof enclosures or remote installation.
Quality Requirements: Oil-free operation mandatory though dew point specifications may relax to -20°C given shorter distribution runs reducing condensation risks. Filtration to 0.1 micron suffices for dental applications though surgical suites maintain 0.01 micron standards.
Stainless steel receivers preferred though some jurisdictions permit coated carbon steel with rigorous inspection programs demonstrating contamination-free performance. Cost pressures drive compromises though patient safety considerations should prevail.
Regulatory Oversight: Local health departments enforce medical gas standards though enforcement intensity varies. Accreditation bodies (Joint Commission, ADA guidelines) establish best practices influencing specifications. Liability concerns motivate conservative approaches exceeding minimum requirements.
Documentation requirements scale with facility size though fundamental traceability principles remain. Material certificates, installation records, and maintenance logs support liability defense if contamination incidents occur.
Food processing facilities face unique challenges balancing compressed air functionality with product safety requirements:
Contamination Risks: Compressed air contacts food directly (package blowing, ingredient conveying, cutting operations) or indirectly (equipment actuation, cleaning systems) creating contamination pathways. Regulatory agencies (FDA, EFSA, local authorities) hold manufacturers liable for air-induced contamination requiring preventive controls.
HACCP (Hazard Analysis Critical Control Point) plans identify compressed air as potential hazard source mandating control measures. Receiver tanks contribute to contamination prevention through appropriate material selection and maintenance practices.
Material Specifications: Stainless steel Type 316L dominates hygienic applications meeting 3-A Sanitary Standards and EHEDG (European Hygienic Engineering and Design Group) guidelines.
Internal surfaces polished to Ra < 0.8 μm enabling effective CIP (clean-in-place) procedures removing biofilm and residues.
Electropolishing enhances passive film quality providing superior corrosion resistance and cleanability compared to mechanical polishing alone. Passivation treatments remove free iron contamination restoring uniform protection. Certification documentation verifies compliance with food contact regulations.
Welded construction eliminates threaded joints creating crevices trapping product residues. Smooth internal profiles prevent stagnation zones where bacteria proliferate. Drainage slopes direct condensate toward low-point drains preventing accumulation.
Design Features: Sloped bottoms (minimum 2% gradient) ensure complete drainage preventing stagnant liquid harboring microorganisms. Low-point drains positioned at absolute lowest locations with self-draining connections eliminating dead legs.
Sanitary fittings (tri-clamp, DIN 11851) replace industrial threads enabling disassembly for inspection and cleaning. Gasket materials comply with FDA 21 CFR 177.2600 for rubber articles intended for repeated use.
Accessibility facilitates visual inspection and swab testing verifying cleanliness. Removable panels or hinged covers enable interior examination without confined space entry procedures.
Cleaning Protocols: CIP systems circulate cleaning solutions (caustic, acid, sanitizer) through receivers periodically removing biofilm and residues. Automated CIP ensures consistent execution though manual cleaning remains common in smaller facilities.
Cleaning frequency depends on usage intensity ranging from daily (high-risk products like dairy, meat) to weekly (lower risk applications). Validation through ATP testing or microbiological swabs confirms cleaning effectiveness.
Documentation of cleaning activities supports regulatory audits and customer quality assessments. Deviations trigger investigations determining root causes and corrective actions.
Dairy Processing: Extreme hygiene requirements demand highest sanitation standards. Air contacts milk products during packaging, conveying, and processing creating direct contamination risks.
Stainless steel receivers with electropolished interiors mandatory. Daily CIP cycles maintain cleanliness. Dew point specifications of -40°C prevent condensation introducing moisture into dry powder processes.
Redundant systems ensure uninterrupted operation critical for continuous processes handling perishable products. Backup receivers automatically engage during maintenance preventing production interruptions spoiling product batches.
Brewing and Beverages: Compressed air agitates fermentation tanks, operates filling equipment, and powers packaging machinery. While not always contacting product directly, air quality affects taste and shelf life. Oil-free compression prevents flavor contamination. Stainless steel receivers eliminate rust particles causing haze or off-flavors.
CO2-rich environments create acidic condensate accelerating corrosion in carbon steel. Stainless steel resists this attack maintaining integrity. Drain systems handle high condensate volumes from humid brewing environments.
Bakery and Confectionery: Air inflates dough, operates depositing equipment, and powers packaging. Direct food contact requires hygienic design though less extreme than dairy. Stainless steel preferred though some facilities accept coated carbon steel with rigorous inspection demonstrating no flaking or contamination.
Temperature variations from oven proximity create thermal cycling stressing coatings. Stainless steel accommodates these swings without degradation. Condensate management proves critical preventing water introduction into dry ingredient handling.
Meat and Poultry Processing: High-humidity environments with washdown procedures create severe corrosion conditions. Stainless steel mandatory resisting constant moisture exposure. Drain systems handle substantial condensate plus washdown water ingress.
Sanitation protocols include high-pressure washing introducing water into air systems if check valves fail. Backflow prevention devices protect receivers from contamination. Regular microbiological testing verifies system cleanliness.
Cold storage areas subject receivers to freezing risks requiring heat tracing or insulated enclosures. Temperature monitoring prevents freeze damage compromising integrity.
Pharmaceutical manufacturing operates under current Good Manufacturing Practice (cGMP)
regulations imposing rigorous quality standards on all systems including compressed air:
Regulatory Framework: FDA 21 CFR Parts 210/211 (US), EU GMP Annex 1, WHO guidelines, and ICH Q7 establish requirements for pharmaceutical production environments. Compressed air classifications range from instrument air (non-product contact) to process air (direct product contact) with escalating quality requirements.
Receiver tanks serving process air applications face strictest scrutiny requiring:
● Stainless steel 316L construction with documented material certificates
● Electropolished internals (Ra < 0.4 μm) validated through surface roughness testing
● Welded sanitary connections with orbital weld procedures qualified per ASME BPE
● Complete documentation packages supporting regulatory submissions
● Change control procedures governing any modifications
Qualification Protocols: Installation Qualification (IQ) verifies equipment matches specifications including material certifications, dimensional inspections, and weld documentation. Operation
Qualification (OQ) demonstrates functional performance through pressure tests, leak checks, and instrumentation calibration.
Performance Qualification (PQ) establishes ongoing compliance through extended monitoring documenting consistent air quality delivery. Sampling plans define testing frequency, parameters measured, and acceptance criteria. Trend analysis identifies deviations triggering investigations.
Requalification occurs periodically (typically annually) or following significant changes ensuring continued compliance. Documentation maintains audit trails demonstrating controlled state throughout equipment lifecycle.
Material Traceability: Every component requires mill certificates verifying chemical composition and mechanical properties. Heat numbers link finished vessels to raw material batches enabling recall if quality issues emerge. Digital databases facilitate rapid retrieval during audits.
Welding consumables similarly tracked with certificates of conformance. Welder qualifications documented proving competency for sanitary welding procedures. Procedure Qualification Records (PQRs) demonstrate welding processes produce compliant joints.
Surface Finish Validation: Surface roughness measurements using profilometers verify electropolishing achieves specified Ra values. Multiple readings across internal surfaces ensure uniformity. Photographic documentation records condition establishing baseline for future comparison.
Passivation verification through ferroxyl testing or copper sulfate tests confirms passive film integrity. Absence of blue coloration indicates successful passivation removing free iron. Documentation supports validation packages.
Biotech facilities producing vaccines, biologics, and cell therapies impose even stricter requirements reflecting product sensitivity:
Sterile Air Requirements: Fermentation processes require sterile compressed air preventing microbial contamination of cultures. Receiver tanks must not introduce bioburden requiring sanitary design and regular sanitization.
Steam-in-place (SIP) capabilities enable thermal sterilization of receivers periodically eliminating accumulated microorganisms. Design accommodates steam injection ports, condensate drains, and temperature monitoring validating sterilization effectiveness.
Materials withstand repeated steam cycling without degradation. Stainless steel proves ideal though gasket materials require careful selection resisting thermal stress. EPDM or PTFE gaskets replace standard elastomers.
Single-Use Integration: Growing adoption of single-use bioreactors reduces but doesn't eliminate compressed air needs. Air still powers actuators, controls environmental chambers, and operates support equipment. Receiver requirements moderate though quality standards remain high.
Flexibility accommodates changing production scales as facilities transition between traditional
stainless steel and single-use technologies. Modular receiver designs enable capacity adjustments matching evolving needs.
Data Integrity: Electronic records of receiver performance, maintenance activities, and quality testing must comply with 21 CFR Part 11 (electronic records) and ALCOA+ principles (Attributable, Legible, Contemporaneous, Original, Accurate plus Complete, Consistent, Enduring, Available).
Audit trails track all data modifications preventing unauthorized changes. Access controls restrict system interactions to authorized personnel. Backup procedures preserve records against loss.
Semiconductor fabrication facilities (fabs) demand extreme air purity levels exceeding most other industries:
Contamination Sensitivity: Sub-micron particle contamination destroys integrated circuits rendering chips non-functional. Compressed air used for wafer handling, chamber purging, and tool actuation must meet ISO 8573 Class 1 specifications:
● Particles: ≤0.1 mg/m³ for 0.1-0.5 micron size range
● Water: ≤0.1 mg/m³ pressure dew point
● Oil: ≤0.01 mg/m³
Receiver tanks must not generate particles through corrosion, coating degradation, or material shedding.
Material Selection: Stainless steel 316L electropolished to Ra < 0.25 μm provides smoothest surfaces minimizing particle generation. Some ultra-critical applications specify 316L VAR (Vacuum Arc Remelted) grades with reduced inclusion content further lowering particle shedding risks.
Internal passivation creates thick protective films preventing corrosion. Regular repassivation maintains protection as films degrade from cleaning cycles. Verification through surface analysis ensures effectiveness.
Welded construction exclusively with automated orbital welding ensuring repeatable quality. 100% radiographic examination plus dye penetrant inspection verifies weld integrity. Smooth internal profiles eliminate turbulence generating particles.
Cleanroom Compatibility: Receivers installed within cleanrooms (Class 1-100) must not compromise air cleanliness. Outgassing from materials releases volatile compounds contaminating sensitive processes. Low-outgassing stainless steel with baked finishes minimizes this risk.
Vibration isolation prevents particle generation from mechanical movement. Seismic bracing maintains stability during earthquakes protecting delicate fab equipment. Fire suppression compatibility ensures receivers don't interfere with suppression systems.
Monitoring and Control: Continuous particle counters monitor air quality downstream of receivers detecting any degradation immediately. Alarms trigger automatic shutdowns preventing contaminated air reaching tools. Data logging supports root cause analysis if excursions occur.
Pressure and temperature sensors track operating conditions correlating with particle generation mechanisms. Trend analysis identifies anomalies preceding failures enabling preventive interventions.
Large fabs consume massive compressed air volumes (10,000-50,000 m³/min) requiring extensive receiver networks:
Centralized vs Distributed: Hybrid approaches combine large central receivers (50,000-200,000liters) providing bulk storage with localized point-of-use units (500-2000 liters) buffering tool-specific demands. Central receivers optimize compressor efficiency while local units isolate disturbances.
Piping design minimizes pressure drops maintaining uniform distribution. Loop configurations provide redundancy preventing single points of failure. Isolation valves enable section maintenance without complete shutdown.
Redundancy Planning: N+1 or N+2 redundancy ensures continuous supply during equipment failures or maintenance. Automatic transfer switches engage backup receivers seamlessly preventing pressure dips affecting tool performance.
Disaster recovery plans address catastrophic events (earthquakes, fires, floods) threatening compressed air supply. Off-site storage agreements provide emergency capacity if primary facilities damaged.
Energy Management: Massive compressed air systems represent significant energy consumers (megawatt-scale). Receiver optimization reduces compressor cycling improving efficiency. Smart controls coordinate receiver charging/discharging with electricity pricing minimizing costs.
Heat recovery from compression warms facility spaces offsetting heating costs. Integrated systems capture waste thermal energy improving overall energy balance. Monitoring quantifies savings supporting sustainability reporting.
EV production creates new compressed air demands differing from traditional automotive:
Battery Production: Dry room environments (dew point <-40°C) prevent moisture damaging battery cells. Compressed air assists electrode coating, cell assembly, and module construction requiring ultra-dry air. Receivers must not introduce moisture through condensation requiring enhanced drying and insulation.
Stainless steel construction prevents corrosion from aggressive electrolyte vapors present in battery manufacturing. Sealed designs prevent vapor ingress compromising air quality. Monitoring detects contamination immediately preventing defective battery production.
Lightweight Materials: Aluminum and composite body structures replace steel requiring different joining techniques. Laser welding, adhesive bonding, and riveting utilize compressed air extensively. Quality requirements balance between automotive precision and electronics sensitivity.
Receiver sizing accommodates pulsed demands from robotic welding cells creating intense short-duration flows. Large storage buffers these spikes enabling efficient compressor operation. Smart controls predict demand patterns optimizing charge/discharge cycles.
Wind turbine and solar panel manufacturing leverage compressed air for various processes:
Wind Turbine Production: Large blade molding operations use compressed air for vacuum bagging, resin infusion, and finishing. Intermittent high-volume demands challenge compressor systems requiring substantial receiver storage.
Outdoor installation sites expose receivers to extreme weather requiring robust protection. Heating systems prevent freezing in cold climates. Corrosion-resistant coatings combat salt spray for offshore wind component manufacturing.
Solar Panel Fabrication: Cleanroom assembly of photovoltaic cells demands particle-free air similar to semiconductor requirements though less extreme. Stainless steel receivers with appropriate filtration serve these applications.
Temperature cycling from outdoor storage creates thermal stresses. Flexible piping connections accommodate expansion/contraction preventing fatigue failures. Monitoring tracks performance across seasonal variations.
Metal and polymer 3D printing utilizes compressed air for powder handling, part cooling, and chamber purging:
Powder Bed Fusion: Inert gas (nitrogen, argon) often replaces air though compressed air powers auxiliary equipment. When air contacts powders, moisture control proves critical preventing oxidation or clumping. Desiccant dryers achieve necessary dew points with receivers providing buffer capacity.
Stainless steel receivers prevent contamination from rust particles mixing with metal powders creating defects. Strict housekeeping prevents cross-contamination between different powder types. Dedicated receivers for each material type eliminate cleaning complexities.
Resin Printing: Compressed air removes excess resin from printed parts requiring oil-free air preventing surface contamination. Receivers must not shed particles or oils compromising part quality. Regular cleaning maintains cleanliness.
Ventilation requirements remove resin vapors from printing areas. Receiver locations consider airflow patterns preventing vapor accumulation around equipment. Explosion-proof fittings address flammable resin concerns.
Criterion | General Mfg | Healthcare | Food & Bev | Pharma/Biotec h | Electronics |
Material | Carbon Steel | SS 316L | SS 316L | SS 316L VAR | SS 316L VAR |
Surface Finish | Coated | Ra <0.4μm | Ra <0.8μm | Ra <0.4μm | Ra <0.25μm |
Certification | ASME/PED | NFPA 99 | 3-A/EHEDG | cGMP/FDA | ISO 8573-1 |
Inspection Freq | Annual | Quarterly | Monthly | Per Validation | Continuous |
Redundancy | Optional | Mandatory | Recommended | Mandatory | N+1/N+2 |
Criterion | General Mfg | Healthcare | Food & Bev | Pharma/Biotec h | Electronics |
Cost Premium | Baseline | 3-4x | 2-3x | 4-5x | 5-6x |
Evaluate selection decisions through risk lens:
Consequence of Failure: Patient harm (healthcare), product recalls (food/pharma), yield loss (electronics), production downtime (manufacturing). Higher consequences justify greater investment in quality.
Probability of Contamination: Direct product contact (high risk) vs indirect equipment actuation (lower risk). Frequency and duration of exposure influence risk levels.
Regulatory Exposure: Heavily regulated sectors (pharma, healthcare) face severe penalties for non-compliance motivating conservative specifications. Less regulated industries balance costs against voluntary standards.
Reputation Impact: Brand damage from quality incidents affects market position disproportionately in consumer-facing industries. B2B industrial customers tolerate occasional issues if communicated transparently.
Initial purchase price represents fraction of lifecycle costs:
Healthcare/Pharma: High initial costs (stainless steel, validation, documentation) offset by reduced contamination risks, regulatory compliance, and liability protection. TCO favors premium specifications despite 3-5x price premiums.
Food & Beverage: Moderate premiums for stainless steel justified through extended service life, reduced maintenance, and brand protection. Hygiene compliance prevents costly recalls and facility shutdowns.
Electronics: Extreme quality requirements make cheapest options false economy. Particle-induced yield losses dwarf receiver cost differences. Investment in ultra-clean systems protects multi-million dollar production outputs.
General Manufacturing: Cost sensitivity drives carbon steel dominance though smart buyers recognize stainless steel value in corrosive environments or critical applications. TCO analysis reveals break-even points where premiums pay back through longevity.
Industry-specific air receiver tank selection requires nuanced understanding of operational requirements, regulatory frameworks, quality standards, and risk profiles unique to each sector.
Generic approaches prove inadequate serving diverse needs ranging from cost-conscious general manufacturing to ultra-stringent semiconductor fabrication.
Successful specifications balance technical requirements against economic realities recognizing that appropriate quality levels vary by application criticality. Healthcare and pharmaceutical sectors rightfully prioritize patient safety and regulatory compliance accepting substantial cost premiums. Food and beverage industries emphasize hygiene and brand protection justifying stainless steel investments. Electronics manufacturing demands extreme purity protecting valuable production outputs. General manufacturing optimizes cost-performance tradeoffs selecting fit-for-purpose solutions.
Engaging qualified suppliers early in specification processes leverages their experience serving similar industries avoiding costly mismatches between equipment capabilities and application demands. Collaboration between end-users, engineering consultants, and manufacturers produces optimal outcomes satisfying technical, regulatory, and economic objectives.
By applying the industry-specific guidance outlined in this guide, organizations select air receiver tanks delivering reliable performance, regulatory compliance, and lifecycle value aligned with their unique operational contexts. The key lies not in universal best practices but in context-appropriate specifications matching equipment characteristics to application requirements through informed decision-making grounded in sector knowledge and risk assessment.
Specializing in pressure vessel manufacturing, we provide reliable, certified, and customized solutions for customers across diverse industries worldwide.
No.268 Xinda Road, High-tech Industrial Park, Longkou City,Shandong Province
Copyright © 2026 Yantai Xinglong Pressure Vessel Manufacturing Co., Ltd All Rights Reserved.


 عربي
 Español
 Русский
