Stay updated with the latest company news, product innovations, exhibition highlights, and industry trends. Explore valuable insights into pressure vessel technologies and global markets.
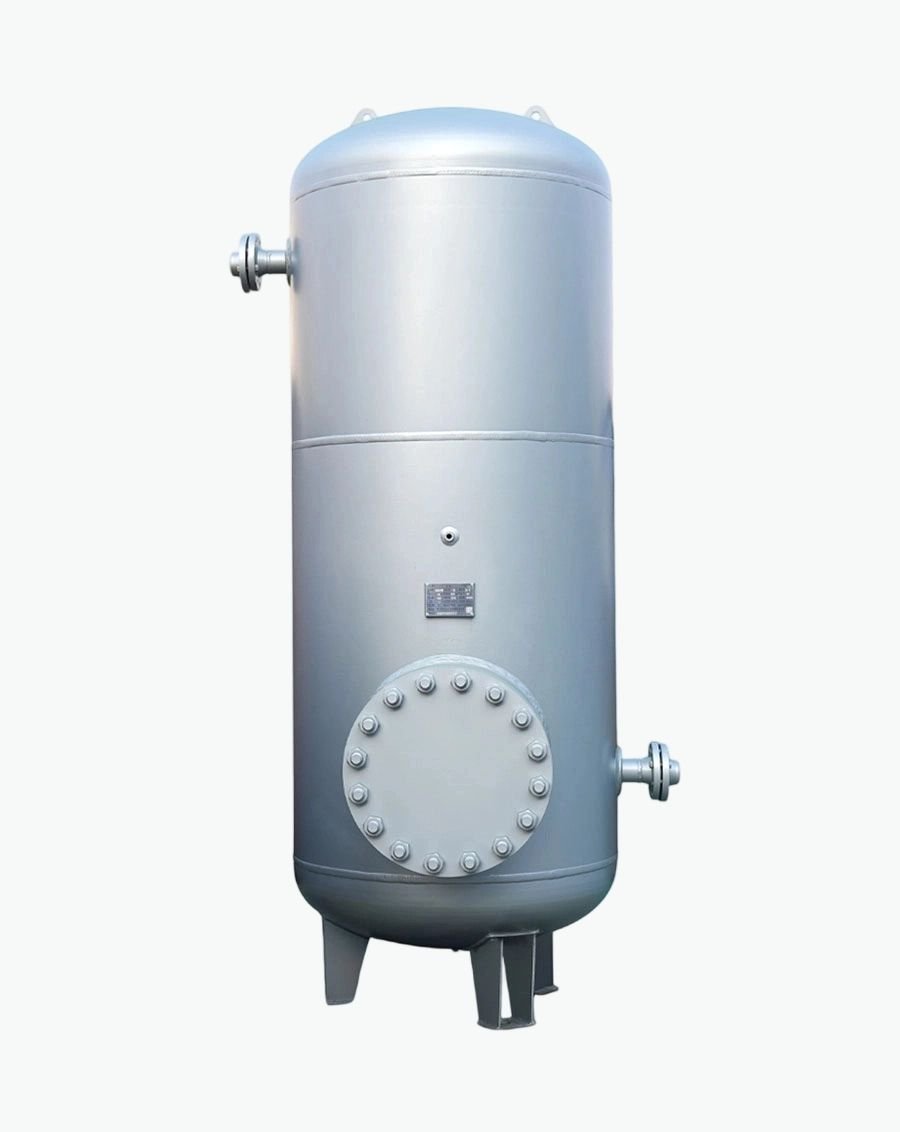
Corrosion represents the single greatest threat to air receiver tank integrity, service life, and operational safety. Internal corrosion from moisture-laden compressed air condensate and external degradation from environmental exposure progressively weaken pressure vessel walls potentially leading to catastrophic failures if left unchecked. Industry data indicates corrosion-related issues account for 60-70% of premature air receiver replacements and contribute significantly to unplanned downtime, safety incidents, and excessive maintenance costs.
Effective corrosion prevention requires systematic approaches combining proper material selection, protective coating systems, condensate management protocols, regular inspection programs, and proactive maintenance practices. While no strategy completely eliminates corrosion risk, comprehensive programs extend service life from typical 10-15 years to 25-30+ years for well-maintained vessels while preserving structural integrity and operational reliability.
This comprehensive guide examines corrosion mechanisms affecting air receiver tanks, evaluates prevention technologies and methodologies, establishes maintenance best practices, and provides actionable frameworks for implementing effective corrosion management programs. By understanding the science behind corrosion processes and applying proven mitigation strategies, facility managers, maintenance teams, and engineering professionals can optimize air receiver lifecycle performance while minimizing total cost of ownership.
Internal corrosion in air receiver tanks results primarily from water vapor condensation creating electrolytic environments conducive to electrochemical metal degradation. Compression processes concentrate ambient humidity with every cubic meter of free air at 20°C and 60% relative humidity containing approximately 10-15 grams of water vapor. When compressed to 8 bar and cooled to ambient temperature, roughly 85-90% of this vapor condenses forming liquid water accumulating in receiver bottoms.
The corrosion process follows electrochemical principles requiring four elements:
1 Anode: Metal surface where oxidation occurs (Fe → Fe²■ + 2e■)
2 Cathode: Adjacent surface where reduction takes place (O■ + 2H■O + 4e■ → 4OH■)
3 Electrolyte: Conductive medium (condensate water) enabling ion transport
4 Electrical Connection: Metallic continuity allowing electron flow
Condensate composition significantly influences corrosion rates. Dissolved oxygen from compressed air accelerates cathodic reactions. Carbon dioxide forms carbonic acid (CO■ + H■O → H■CO■) lowering pH to 4-5 range enhancing metal dissolution. Trace contaminants including compressor lubricant carryover, atmospheric pollutants (SO■ , NOx, chlorides), and process chemicals further aggravate corrosion through acidic formation or localized attack mechanisms.
Typical internal corrosion patterns include:
Uniform General Corrosion: Even material loss across wetted surfaces progressing at 0.05-0.2mm/year depending on conditions. While predictable and manageable through corrosion allowances, cumulative thickness loss eventually compromises pressure containment requiring replacement.
Pitting Corrosion: Localized aggressive attack creating deep cavities penetrating walls rapidly despite minimal overall material loss. Chloride ions, stagnant water pockets, and coating defects initiate pits that propagate autocatalytically as acidic conditions develop within confined spaces.
Pitting proves particularly dangerous as significant wall thinning may occur undetected until failure.
Crevice Corrosion: Occurs at gasketed joints, threaded connections, support attachments, and areas where debris accumulates creating oxygen-depleted zones. Differential aeration cells establish between crevice interior (anodic) and exposed surfaces (cathodic) driving aggressive localized
attack. Design modifications eliminating crevices substantially reduce this corrosion mode.
Microbiologically Influenced Corrosion (MIC): Bacteria including sulfate-reducing organisms thrive in warm, moist receiver environments producing corrosive metabolic byproducts. Biofilms create differential concentration cells accelerating localized attack. MIC manifests as irregular pitting beneath slimy deposits often misdiagnosed as simple mechanical damage.
Temperature effects prove complex. Elevated temperatures increase reaction kinetics accelerating corrosion rates according to Arrhenius relationships (typically doubling per 10°C rise). However, higher temperatures also reduce dissolved oxygen concentrations partially offsetting acceleration. Operating ranges of 20-40°C common in receivers represent moderate corrosion risk zones.
External surfaces face diverse environmental challenges depending on installation location:
Atmospheric Corrosion: Ambient humidity, temperature cycling, and airborne contaminants drive external degradation. Coastal locations present severe chloride exposure from salt spray causing rapid pitting even on coated carbon steel. Industrial atmospheres contain SO■ , NOx, and particulate matter forming acidic deposits when combined with moisture. Rural environments prove less aggressive though organic acids from vegetation decomposition create mild corrosion risks.
ISO 9223 classifies atmospheric corrosivity into categories C1 (very low) through C5 (very high) guiding coating system selection. Most industrial facilities fall within C3-C4 ranges requiring robust protection systems.
Galvanic Corrosion: Dissimilar metal contacts create electrochemical cells driving accelerated degradation of less noble materials. Common scenarios include stainless steel fittings on carbon steel receivers, copper drain valves, aluminum nameplates, and steel supports contacting galvanized structures. Potential differences exceeding 0.25V between metals in conductive environments trigger significant galvanic currents.
Prevention requires electrical isolation through non-conductive gaskets, insulating coatings, or sacrificial anodes protecting critical components. Material compatibility charts guide appropriate pairing selections avoiding problematic combinations.
Stray Current Corrosion: Electrical leakage from nearby equipment, welding operations, or cathodic protection systems on adjacent structures induces electrolytic corrosion on receivers acting as unintended current paths. DC stray currents prove particularly damaging causing rapid metal dissolution at anodic discharge points. Proper grounding practices and electrical isolation mitigate these risks.
Mechanical Damage Leading to Corrosion: Impact damage during installation, maintenance activities, or accidental collisions compromise protective coatings exposing bare metal to corrosive environments. Scratches, dents, and abrasions create initiation sites for localized attack that spreads beneath intact coatings through undercutting mechanisms. Prompt repair of mechanical damage prevents corrosion propagation.
Internal coatings provide barrier protection isolating metal surfaces from corrosive condensate. Selection criteria include chemical resistance, adhesion strength, application feasibility, cure requirements, and regulatory compliance for specific applications.
Epoxy Phenolic Linings: Most common internal protection offering excellent chemical resistance across broad pH ranges (2-12). Two-component formulations provide superior adhesion and impermeability compared to single-pack alternatives. Application requires thorough surface preparation (Sa 2.5 blast profile minimum), controlled temperature (15-25°C) and humidity (<85% RH) during curing, and adequate ventilation removing solvent vapors.
Typical specifications call for 300-500 micron dry film thickness applied in multiple coats ensuring pinhole-free coverage. Holiday detection testing using high-voltage spark testers identifies coating discontinuities requiring touch-up before commissioning. Properly applied epoxy linings extend carbon steel service life 15-20 years in moderate service.
Limitations include temperature restrictions (maximum 80°C continuous service), UV sensitivity requiring darkness during storage, and difficulty repairing damaged areas in-service necessitating complete relining for extensive deterioration.
Food-Grade Epoxy Formulations: FDA 21 CFR 175.300 compliant coatings serve food, beverage, and pharmaceutical applications where incidental product contact occurs. These formulations eliminate toxic components (amines, heavy metals) while maintaining protective performance. Certification documentation supports regulatory audits and customer quality requirements.
Application procedures mirror standard epoxy protocols though cleanliness standards increase dramatically. Cleanroom conditions during application prevent particulate contamination. Post-cure swab testing verifies absence of extractable compounds meeting purity specifications.
Polyurethane Linings: Offer superior abrasion resistance compared to epoxies beneficial for receivers experiencing turbulent flow or particle impingement. Flexibility accommodates thermal cycling stresses without cracking. However, chemical resistance proves inferior to epoxies particularly regarding acidic condensate limiting applicability.
Two-component polyurethanes require precise mixing ratios and pot life management preventing premature gelation. Moisture sensitivity during application demands strict humidity control. Costs typically 20-30% higher than epoxy alternatives.
Glass Flake Reinforced Coatings: Incorporate microscopic glass platelets creating tortuous pathways blocking permeant diffusion. Enhanced barrier properties enable thinner films achieving equivalent protection to conventional coatings. Excellent chemical resistance and temperature tolerance (up to 120°C) suit demanding applications.
Application complexity increases due to viscosity requiring specialized spray equipment. Surface preparation standards remain critical as glass flakes cannot bridge substrate defects. Premium pricing reflects performance advantages though lifecycle cost benefits justify investments for aggressive service conditions.
External protection combats atmospheric corrosion through multi-layer systems combining complementary functions:
Zinc-Rich Primers: Provide cathodic (sacrificial) protection where zinc particles electrically connect to steel substrate corroding preferentially shielding underlying metal. Organic zinc-rich primers (epoxy or polyurethane binders) offer easier application than inorganic silicate variants though slightly reduced protection longevity.
Typical loading requires 85-92% zinc by weight in dry film ensuring electrical continuity. Thickness specifications range 60-80 microns providing adequate sacrificial reserve. Zinc consumption rates approximate 0.1 -0.3 microns/year in moderate atmospheres suggesting 10-20 year protection duration before depletion.
Epoxy Intermediate Coats: Build barrier protection adding thickness and chemical resistance. High-build epoxy formulations enable 150-200 micron layers in single applications reducing coat count. Excellent adhesion to zinc primers and topcoats creates cohesive system integrity.
Chemical resistance encompasses mild acids, alkalis, solvents, and salts encountered in industrial environments. Temperature tolerance typically -20°C to 80°C accommodating most outdoor installations. Gloss retention proves moderate though acceptable beneath topcoats.
Polyurethane Topcoats: Deliver UV resistance, color retention, and aesthetic finish protecting underlying layers from solar degradation. Aliphatic polyurethanes resist yellowing maintaining appearance throughout service life. Gloss levels (semi-gloss to high-gloss) facilitate cleaning and inspection visibility.
Thickness specifications of 50-75 microns balance protection against application economy. Multiple color options enable coding schemes identifying system contents, pressure ratings, or inspection status per facility conventions. Blue remains standard for compressed air though custom colors support corporate branding.
Total System Performance: Combined primer-intermediate-topcoat systems achieve 200-300 micron total dry film thickness providing comprehensive protection. Expected service life ranges 10-15 years in C3 atmospheres, 7-10 years in C4 industrial zones, and 5-7 years in C5 coastal/marine environments before recoating required.
Surface preparation proves critical determining coating longevity. Abrasive blasting to Sa 2.5 (near-white metal) removes rust, mill scale, and contaminants creating optimal anchor profile (50-75 microns) for coating adhesion. Power tool cleaning achieves St 3 standard suitable for maintenance repainting though inferior to blast cleaning for initial applications.
Rigorous inspection protocols verify coating quality before commissioning:
Visual Examination: Identifies runs, sags, orange peel, pinholes, and inadequate coverage. Trained inspectors assess uniformity, color consistency, and surface defects under adequate lighting (minimum 500 lux). Documentation includes photographic records supporting warranty claims and future reference.
Dry Film Thickness Measurement: Magnetic gauges (for carbon steel substrates) or eddy current instruments (non-ferrous) verify thickness meets specifications. Multiple readings per square meter ensure representative sampling. Statistical analysis confirms compliance with minimum/maximum tolerances (typically ±20% of nominal).
Holiday Detection: High-voltage spark testers (5-15 kV depending on thickness) identify pinholes and thin spots compromising barrier integrity. Detected holidays marked for touch-up before final acceptance. Critical applications require 100% holiday testing while general service accepts statistical sampling.
Adhesion Testing: Cross-hatch cuts followed by tape pull-off evaluate coating bond strength. ASTM D3359 specifies procedures with rating scales from 0B (complete removal) to 5B (no detachment). Minimum acceptable ratings typically 4B indicating strong adhesion resistant to undercutting corrosion.
Cure Verification: Solvent rub tests assess polymerization completeness. Methyl ethyl ketone (MEK) double-rub procedures determine whether coatings achieved full cure resisting solvent attack.
Incomplete curing leads to soft films susceptible to mechanical damage and chemical penetration.
Third-party coating inspectors certified through NACE or SSPC programs provide objective verification independent of application contractors. Their expertise proves valuable for critical installations where coating failure consequences justify professional oversight costs.
Effective condensate removal prevents water accumulation driving internal corrosion. Drain system design considerations include:
Automatic Drain Valves: Electronic timer-controlled or level-sensing drains remove accumulated condensate without manual intervention. Timer units discharge predetermined volumes at set intervals regardless of actual accumulation risking either excessive air waste (if timed too frequently) or inadequate drainage (if intervals too long). Level-sensing floats activate only when water reaches threshold optimizing efficiency though mechanical floats may stick requiring periodic testing.
Zero-loss drains utilizing capacitive sensors detect water presence activating brief discharge pulses minimizing compressed air waste. Initial costs exceed conventional drains 3-5x though energy savings from reduced air loss achieve payback within 12-18 months for typical installations.
Installation positioning at receiver lowest point ensures gravity-driven drainage. Multiple drains benefit large horizontal receivers preventing dead zones where water pools between drain locations. Drain line sizing (minimum 15mm diameter) prevents restriction during rapid discharge events.
Manual Drain Valves: Serve as backups to automatic systems or primary drainage in facilities preferring hands-on control. Ball valves prove superior to gate valves for frequent operation providing quick quarter-turn actuation and visual position indication. Regular scheduling (daily or shift-based) ensures consistent execution though human reliability varies requiring supervision and accountability measures.
Drain valve materials must resist corrosion from condensate exposure. Stainless steel or brass construction outlasts carbon steel alternatives particularly in aggressive environments. Thread sealants compatible with compressed air service prevent leakage around valve stems.
Drain Line Routing: Discharge lines route to appropriate collection points preventing environmental contamination or slip hazards. Oil-water separators treat lubricant-contaminated condensate meeting regulatory discharge requirements. Direct sewer connections violate environmental regulations in most jurisdictions requiring pretreatment verification.
Insulated drain lines prevent freezing in cold climates avoiding blockages compromising drainage effectiveness. Heat tracing maintains flow during extreme cold though adds complexity and energy consumption. Sloped piping (minimum 1:100 gradient) ensures complete drainage preventing standing water accumulation in lines themselves.
Receiver corrosion prevention begins upstream through effective moisture removal before air enters storage:
Aftercoolers: Reduce compressed air temperature immediately following compression promoting initial condensate separation. Typical cooling from 150°C discharge to 35-40°C removes 60-70% of water vapor. Larger heat exchange surfaces and lower approach temperatures enhance moisture removal though diminishing returns apply below 30°C.
Regular aftercooler maintenance ensures optimal performance. Fouled heat transfer surfaces reduce cooling effectiveness allowing more moisture into receivers. Tube cleaning, fan belt tension checks, and coolant level monitoring comprise essential maintenance tasks.
Refrigerated Dryers: Further cool air to 3-5°C dew point removing additional 25-30% of remaining moisture. Pressure dew point specifications of 3°C mean condensate forms only if air temperature drops below this threshold downstream. Properly sized and maintained refrigerated dryers significantly reduce receiver water loading extending coating life.
Energy consumption represents trade-off against corrosion prevention benefits. Modern units achieve specific power of 0.08-0.12 kW per m³/min balancing efficiency against drying performance. Variable capacity models modulate cooling based on actual load improving part-load efficiency.
Desiccant Dryers: Achieve ultra-low dew points (-40°C or below) necessary for critical applications though overkill for general industrial service. Regeneration energy requirements (heatless, heated, or blower purge) substantially increase operating costs. Over-drying wastes energy without proportional corrosion prevention benefits for standard receivers.
Appropriate dryer selection matches dew point requirements to actual application needs rather than specifying unnecessarily low levels. ISO 8573-1 classes guide selection with Class 4 (3°C PDP) adequate for most manufacturing while Classes 1-2 serve instrumentation and sensitive processes.
Continuous monitoring ensures condensate management systems function effectively:
Water Accumulation Tracking: Measuring discharged condensate volumes quantifies moisture loading trends. Sudden increases indicate upstream treatment failures (dryer malfunction, aftercooler fouling) requiring investigation. Gradual increases suggest seasonal humidity changes or production volume growth.
Automated flow meters on drain lines provide continuous data logging enabling trend analysis. Comparison against theoretical moisture content calculations validates system performance identifying deviations requiring corrective action.
Drain Valve Testing: Regular functional tests verify automatic drains operate correctly. Manual override activations confirm solenoid response and valve movement. Float mechanism inspections check for sticking, corrosion, or debris interference preventing proper operation.
Testing frequency depends on criticality. Monthly tests suffice for general service while critical applications warrant weekly verification. Test logs document performance history supporting preventive maintenance scheduling and warranty claims.
Air Loss Quantification: Zero-loss drain claims require verification through flow measurement comparing discharge events against expected water volumes. Excessive air discharge indicates faulty sensors, incorrect settings, or valve leakage wasting energy. Optimized drains discharge only liquid water with minimal entrained air.
Ultrasonic leak detectors identify drain valve leaks during closed periods. Persistent hissing sounds indicate seat damage or debris preventing tight shutoff requiring repair or replacement. Quantified leak rates enable cost-benefit analysis justifying premium drain upgrades.
Regular visual examinations identify early-stage corrosion enabling timely intervention before significant damage occurs:
External Inspections: Monthly walkthroughs examine coating condition looking for rust staining, blistering, peeling, or mechanical damage. Particular attention focuses on weld seams, nozzle connections, support attachments, and low points where water collects. Photographic documentation tracks deterioration progression supporting maintenance planning.
Rust staining running downward from specific locations indicates active corrosion beneath coating requiring investigation. Blistering suggests moisture entrapment between coating layers or substrate creating osmotic pressure lifting films. Mechanical damage from impacts, abrasion, or thermal stress exposes bare metal needing prompt repair.
Internal Inspections: Annual internal examinations during scheduled shutdowns provide direct assessment of internal condition. Confined space entry procedures mandate atmospheric testing, ventilation, lockout/tagout, and standby personnel ensuring safe access.
Visual examination identifies coating condition, corrosion patterns, pitting severity, and sediment accumulation. Probe measurements quantify remaining wall thickness at representative locations comparing against original specifications. Ultrasonic thickness gauging provides precise readings without coating removal though couplant application requires surface preparation.
Photographic records document condition establishing baseline for future comparison. Grid mapping divides interior into sections ensuring comprehensive coverage preventing overlooked areas.
Particular scrutiny applies to water line regions experiencing alternating wet-dry cycles accelerating corrosion.
Documentation Standards: Inspection forms capture standardized data including date, inspector name, weather conditions, observations, measurements, photographs, and recommendations. Digital platforms enable easy retrieval, trend analysis, and report generation supporting maintenance decision-making.
Condition rating scales (e.g., 1-5 with 5 being excellent) simplify communication though detailed narrative descriptions provide necessary context. Severity classifications (minor, moderate, severe, critical) prioritize corrective actions allocating resources effectively.
Advanced NDE techniques supplement visual inspections providing quantitative data on subsurface conditions:
Ultrasonic Thickness Testing: Measures remaining wall thickness through coatings without surface preparation. Piezoelectric transducers send sound pulses reflecting from back wall with transit time correlating to thickness. Accuracy ±0.1mm suffices for corrosion assessment though couplant application and surface curvature affect readings.
Multiple readings per square meter create thickness maps revealing variation patterns. Minimum thickness locations identify areas requiring reinforcement or monitoring. Comparison against original thickness calculates corrosion rates projecting remaining life.
Phased array ultrasonics enable rapid scanning covering larger areas efficiently. Automated crawlers move transducers systematically recording thousands of data points generating detailed corrosion profiles. Investment justified for large receivers or critical service applications.
Radiographic Examination: X-ray or gamma ray imaging reveals internal defects including cracks, voids, and severe wall thinning. Particularly useful for weld inspection verifying joint integrity. Safety precautions limit radiation exposure requiring licensed operators and controlled access zones.
Digital radiography replaces film providing immediate images with enhanced contrast adjustment capabilities. Computed tomography (CT) scanning produces three-dimensional reconstructions enabling volumetric defect characterization though costs prohibit routine application.
Magnetic Particle Inspection: Detects surface and near-subsurface cracks in ferromagnetic materials. Magnetic field application followed by iron particle suspension reveals flux leakage at discontinuities indicating crack presence. Effective for weld examination and stress corrosion cracking detection.
Limitations include requirement for ferromagnetic materials (ineffective for stainless steel or composites), surface preparation needs, and interpretation subjectivity. Qualified examiners undergo certification ensuring competent evaluation.
Eddy Current Testing: Electromagnetic induction detects surface cracks and measures coating thickness on conductive substrates. Portable instruments enable rapid screening though depth penetration limits restrict use to near-surface defects. Calibration standards matching material properties ensure accurate readings.
Particularly valuable for inspecting stainless steel receivers where magnetic methods fail. Coil frequency selection balances sensitivity against penetration depth optimizing defect detection for specific applications.
Regulatory codes and industry best practices establish minimum inspection intervals:
ASME Requirements: Jurisdictional regulations typically mandate external inspections annually and internal inspections every 3-5 years depending on service severity. Hydrostatic testing every 5-10 years validates structural integrity though frequency varies by jurisdiction and service history.
Owner-user inspection programs per ASME Section V allow extended intervals based ondocumented condition monitoring demonstrating stable corrosion rates. Risk-based inspection (RBI) methodologies optimize frequencies focusing resources on highest-risk vessels.
European PED Guidelines: Notified bodies specify inspection intervals during initial certification typically ranging 2-5 years for internal examinations. Continued compliance requires adherence to prescribed schedules though extensions possible through technical justification demonstrating adequate condition monitoring.
Member state variations exist with some countries imposing stricter requirements than others. Harmonization efforts continue though national authorities retain enforcement discretion.
Risk-Based Inspection Approaches: RBI combines probability of failure (corrosion rate, inspection history, operating conditions) with consequence of failure (pressure, volume, location, contents) prioritizing inspection resources. High-risk vessels receive frequent thorough examinations while low-risk units extend intervals reducing unnecessary downtime.
Software tools facilitate RBI calculations incorporating industry databases and site-specific data. Regular updates refine predictions as new inspection data becomes available improving accuracy over time.
Structured preventive maintenance preserves receiver condition preventing unexpected failures:
Weekly Tasks:
● Verify automatic drain operation observing discharge during manual test cycle
● Check pressure gauge readings comparing inlet/outlet identifying blockages
● Inspect external surfaces for new damage, corrosion signs, or coating deterioration
● Confirm safety relief valve tags current and unobstructed
Monthly Tasks:
● Manually drain receiver ensuring complete water removal even if automatic drains appear functional
● Clean strainers or filters in inlet/outlet connections preventing flow restriction
● Test drain valve operation manually overriding automatic controls
● Inspect support structures for corrosion, loose bolts, or foundation settlement
● Review inspection logs identifying trends requiring attention
Quarterly Tasks:
● Conduct thorough external coating examination documenting any deterioration
● Measure wall thickness at representative locations tracking corrosion progression
● Inspect internal condition if accessible without confined space entry (through nozzles)
● Calibrate pressure gauges and transmitters ensuring accurate readings
● Test safety relief valves verifying opening pressure and reseating characteristics
Annual Tasks:
● Perform comprehensive internal inspection during scheduled shutdown
● Conduct ultrasonic thickness survey mapping corrosion distribution
● Evaluate coating condition internally and externally planning repairs
● Recalibrate all instrumentation including pressure switches and level sensors
● Update inspection records and condition assessments
● Review maintenance history identifying recurring issues requiring root cause analysis
Five-Year Tasks:
● Complete hydrostatic testing per regulatory requirements validating structural integrity
● Consider internal recoating if corrosion rates indicate approaching minimum thickness
● Evaluate replacement economics comparing continued maintenance against new vessel investment
● Update risk assessments incorporating latest inspection data and operating experience
Maintenance task optimization balances thoroughness against resource availability. Computerized maintenance management systems (CMMS) schedule tasks automatically generating work orders and tracking completion. Mobile applications enable field technicians accessing procedures, recording findings, and capturing photos streamlining documentation.
When inspections reveal corrosion or damage, systematic corrective actions restore integrity:
Minor Surface Rust: Light surface oxidation without significant metal loss requires cleaning and touch-up coating. Wire brushing or light abrasive blasting removes rust converting to stable surface. Primer application followed by topcoat restores protection. Monitor closely for recurrence indicating underlying issues.
Localized Pitting: Isolated pits not exceeding 50% wall thickness permit local repair. Grinding removes pit creating smooth transition blending into surrounding material. Weld buildup restores thickness if needed followed by grinding flush. Recoat repaired area matching surrounding system. Increase inspection frequency monitoring for additional pitting.
Extensive Corrosion: Widespread thinning approaching minimum required thickness necessitates major intervention. Options include:
● Internal recoating extending life if sufficient thickness remains
● Weld overlay reinforcing thin areas though heat input concerns require engineering review
● Replacement planning if thickness insufficient for safe continued operation
Engineering assessment determines whether repairs meet code requirements or replacement proves more economical. Temporary derating (reduced MAWP) may allow continued operation while planning replacement though operational impacts require consideration.
Coating Failure: Blistering, peeling, or delamination indicates coating system breakdown requiring rehabilitation. Complete removal via abrasive blasting to bare metal followed by reapplication proves most reliable though costly. Spot repairs risk premature failure at boundaries between old and new coatings.
Root cause analysis identifies failure mechanisms preventing recurrence. Common causes include inadequate surface preparation, moisture entrapment during application, chemical incompatibility, or mechanical damage. Addressing underlying causes improves longevity of replacement coatings.
Adequate spare parts availability minimizes downtime during repairs:
Critical Spares: Maintain inventory of drain valves, pressure gauges, safety relief valves, and gaskets enabling rapid replacement. Standardization across facility reduces variety simplifying inventory management. Vendor agreements ensure emergency supply within 24-48 hours for items not stocked.
Coating Materials: Stock touch-up coating kits matching installed systems enabling prompt repair of minor damage. Proper storage (temperature-controlled, sealed containers) preserves material quality. Shelf life monitoring prevents use of expired products compromising protection.
Documentation Access: Maintain readily accessible copies of original drawings, material certificates, coating specifications, and inspection records supporting repair decisions. Digital archives enable remote access facilitating contractor coordination and regulatory compliance verification.
Inventory optimization balances carrying costs against stockout risks. ABC analysis categorizes items by criticality and usage frequency guiding stocking levels. Vendor-managed inventory arrangements shift responsibility to suppliers for commodity items while maintaining service levels.
Understanding corrosion costs motivates preventive investment:
Direct Costs:
● Emergency repair labor (overtime premiums, expedited shipping)
● Replacement vessel purchase and installation
● Production downtime losses during unplanned shutdowns
● Environmental cleanup from leaked condensate or coating materials
● Regulatory fines for safety violations or environmental non-compliance
Indirect Costs:
● Reputation damage from safety incidents affecting customer confidence
● Increased insurance premiums following claims
● Engineering investigation expenses determining root causes
● Management time diverted addressing crisis rather than strategic initiatives
● Employee morale impacts from safety concerns
Typical unplanned receiver replacement costs 2-3x planned replacement due to emergency pricing, expedited delivery, and overtime labor. Production downtime adds substantial losses particularly for continuous processes where compressed air interruptions halt entire facilities.
Investment in comprehensive corrosion prevention yields attractive returns:
Initial Investment:
● Quality coating systems: $50-100 per square meter
● Automatic drain upgrades: $500-2,000 per receiver
● Inspection equipment (ultrasonic gauge, cameras): $2,000-5,000
● Training programs: $1,000-3,000 per technician
Annual Operating Costs:
● Preventive maintenance labor: 20-40 hours per receiver
● Coating touch-up materials: $200-500 per receiver
● Inspection services (if outsourced): $1,000-3,000 per receiver
● Drain valve energy consumption: $100-300 per receiver
Savings Realized:
● Extended service life: 10-15 additional years avoiding $5,000-15,000 replacement costs
● Reduced emergency repairs: Avoid $2,000-5,000 per incident
● Energy savings from zero-loss drains: $300-800 annually per receiver
● Downtime avoidance: Priceless for critical operations
Payback periods typically 2-4 years for comprehensive programs with ongoing annual savings thereafter. Lifecycle cost comparisons clearly favor preventive approaches over reactive maintenance though upfront budget allocation requires justification.
Optimizing maintenance budgets across receiver fleets:
Risk-Based Prioritization: Allocate disproportionate resources to high-risk receivers (critical service, aggressive environments, known corrosion issues) while maintaining minimum standards for low-risk units. This approach maximizes overall fleet reliability within budget constraints.
Phased Implementation: Roll out improvements gradually starting with worst-condition receivers demonstrating quick wins building support for broader programs. Early successes generate momentum securing funding for subsequent phases.
Vendor Partnerships: Long-term service contracts with qualified coating applicators and inspection firms secure preferential pricing while ensuring consistent quality. Volume commitments leverage purchasing power though flexibility provisions accommodate changing needs.
Technology Investments: Automated monitoring systems reduce manual inspection labor while providing continuous data enabling predictive interventions. Initial costs offset by labor savings and improved reliability justifying capital expenditure approvals.
A mid-sized automotive supplier experienced repeated receiver failures averaging 8-year service life due to aggressive internal corrosion. Root cause analysis revealed inadequate condensate drainage, poor coating quality, and absent inspection programs.
Intervention program included:
● Complete internal recoating with high-performance epoxy phenolic lining
● Installation of zero-loss electronic drains on all receivers
● Implementation of quarterly ultrasonic thickness monitoring program
● Technician training on corrosion recognition and preventive maintenance
● Upstream refrigerated dryer upgrade reducing moisture loading
Results after five years:
● Zero unplanned failures compared to previous 2-3 annually
● Measured corrosion rates decreased 80% from 0.15 mm/year to 0.03 mm/year
● Projected service life extended from 8 years to 25+ years
● Energy savings from zero-loss drains: $1,200 annually per receiver
● Total program cost: $45,000; avoided replacement costs: $120,000; net savings: $75,000 plus reliability improvements
Specialty chemical manufacturer faced severe external corrosion on receivers installed in coastal location with salt spray exposure. Standard coating systems failed within 3-4 years requiring frequent recoating disrupting operations.
Solution implemented:
● Upgrade to multi-coat system with zinc-rich primer, high-build epoxy intermediate, and fluoropolymer topcoat providing superior salt spray resistance
● Install protective enclosures shielding receivers from direct salt exposure
● Implement monthly external inspection program with photographic documentation
● Apply sacrificial zinc anodes at critical locations experiencing galvanic corrosion
● Establish coating repair protocol addressing mechanical damage within 48 hours
Outcomes achieved:
● Coating service life extended from 4 years to 12+ years
● Recoating frequency reduced 67% saving $15,000 annually in maintenance costs
● Eliminated safety incidents from sudden coating failures
● Improved facility appearance supporting customer audit scores
● Payback period: 18 months from reduced maintenance frequency
Conclusion
Effective corrosion prevention and maintenance for air receiver tanks requires systematic integration of proper material selection, quality coating systems, efficient condensate management, rigorous inspection programs, and proactive maintenance practices. While corrosion cannot be completely eliminated, comprehensive management programs extend service life two to three times beyond neglected equivalents while preserving structural integrity and operational reliability.
Success demands organizational commitment allocating adequate resources for preventive activities rather than reacting to failures after they occur. Training programs build internal expertise enabling early problem identification and appropriate corrective actions. Documentation systems track condition trends supporting data-driven maintenance decisions optimizing resource allocation.
Economic analysis consistently demonstrates attractive returns from corrosion prevention investments through extended equipment life, reduced emergency repairs, energy savings, and downtime avoidance. While initial costs appear substantial, lifecycle cost comparisons clearly favor preventive approaches delivering superior value throughout receiver operational lifespan.
By implementing the best practices outlined in this guide, industrial facilities transform air receiver corrosion from unpredictable threat into manageable condition maintaining compressed air system reliability, safety, and efficiency for decades of productive service. The key lies not in any single technology or procedure but in holistic integration of complementary strategies creating defense-in-depth protecting these critical pressure vessels against progressive degradation.
Specializing in pressure vessel manufacturing, we provide reliable, certified, and customized solutions for customers across diverse industries worldwide.
No.268 Xinda Road, High-tech Industrial Park, Longkou City,Shandong Province
Copyright © 2026 Yantai Xinglong Pressure Vessel Manufacturing Co., Ltd All Rights Reserved.


 عربي
 Español
 Русский
