Explore our completed pressure vessel projects across diverse industries, showcasing engineering expertise, manufacturing excellence, and reliable project delivery.
Content status: representative engineering application case for website planning. It does not identify or claim a named customer's completed order. All vessel values are preliminary engineering reference values. Final manufacture requires confirmed duty conditions, applicable jurisdiction, approved drawings and formal pressure-vessel calculations.
Compressor Capacity | Working Pressure | Receiver Capacity | Arrangement |
11.0 m3/min FAD / approx. 90 kW | 9.0 bar(g) | 2,500 L | Vertical |
This representative engineering application case is developed for a pet bottle blowing facility where compressed air is a production utility rather than a secondary convenience. Typical users include preform conveying, stretch-blow molding, high-pressure bottle blowing, low-pressure controls and packaging auxiliaries. The purpose of the receiver is not simply to add nominal storage volume. It is to create controlled pneumatic capacitance between compressor supply and plant demand so that short flow mismatches do not immediately appear as a pressure disturbance at the user header. The reference plant has strong pulsed demand at each blow cycle with very high instantaneous flow relative to average consumption.
Because of that operating pattern, receiver selection has to be coordinated with compressor capacity, pressure set points, air treatment, piping resistance, and the minimum pressure accepted by the production equipment. In this case, the selected compressor concept delivers approximately 11.0 m3/min FAD at 9.0 bar(g), and the receiver provides 2,500 L of nominal storage in a vertical arrangement. The engineering objective is stable utility performance rather than maximum tank size. The plant needs oil-free, dry compressed air appropriate for high-pressure bottle-forming service and clean pneumatic controls. A receiver that is too small can allow rapid pressure movement and excessive control activity; a receiver that is much larger than necessary can occupy valuable space and slow system response during filling. The case therefore balances usable storage, compressor control behavior and installation constraints. It also treats the receiver as a pressure vessel requiring formal code design, material traceability, protected nozzles, reliable drainage and correctly sized safety devices. The stated vessel dimensions and thickness are preliminary reference values for project planning. They demonstrate how a custom pressure-vessel manufacturer can coordinate the mechanical package around a defined compressor duty, but they are not a substitute for the final design calculation required by the governing pressure-vessel code.
The pet bottle blowing facility uses compressed air for preform conveying, stretch-blow molding, high-pressure bottle blowing, low-pressure controls and packaging auxiliaries. These users do not consume air at a perfectly constant rate. The engineering basis assumes an average demand of about 7.8 m3/min, a light-load condition near 2.9 m3/min and short combined peaks approaching 13.8 m3/min. Those numbers are intentionally expressed as a demand range instead of a single nameplate value because receiver performance is determined by the difference between instantaneous demand and instantaneous compressor delivery. When the peak rises above compressor output, stored air supplements the compressor for a short period.
When demand falls, the receiver accepts excess delivery and slows the pressure rise that would otherwise force a rapid control reaction. The consequence of poor pressure stability in this application is practical: insufficient storage can cause blow-pressure decay, bottle-quality variation and unnecessary booster cycling. For that reason, the receiver is located where its stored volume can actually influence the pressure sensor and the users that need support. A large tank connected through an undersized branch line can behave like a small tank because air cannot move into or out of it quickly enough. The project therefore links receiver volume to branch-line size, isolation valves, check valves, dryer pressure drop and the location of the compressor control transducer. During a real site audit, second-by-second pressure and flow logging would be preferred. Where that data is unavailable, production cycles, machine counts and peak-event timing provide the next-best basis for defining a useful storage requirement.
The representative customer requirement is to maintain a useful production header of approximately 8.5 bar(g) while allowing enough upstream pressure to cover treatment and distribution losses. Compressor discharge pressure is therefore set at 9.0 bar(g), not because higher pressure is automatically desirable, but because the system has to deliver the required pressure at the most demanding user after filters, dryer, valves and piping are included. The expected operating environment is high-speed packaging halls where high-pressure piping and safety segregation require careful layout, and the receiver is specified for an ambient range of -10 to +45 C. The mechanical package also needs maintenance access for the drain, safety valve, pressure gauge and isolation points, along with lifting and foundation provisions compatible with the vessel weight of about 1,350 kg.
Before final design, the customer or system integrator would normally provide the compressor data sheet, FAD at the selected pressure, operating pressure band, maximum discharge temperature, air-treatment sequence, required dew point, pipe sizes, preferred nozzle directions, available floor area, lifting restrictions and jurisdictional code requirements. These inputs are more useful than a simple request for a '2,500 L tank' because they define how the vessel must work inside the system. The custom-manufacturing scope then converts those functional requirements into a general arrangement drawing, nozzle schedule, support design, material specification and inspection plan. This engineering review is especially important when the receiver must replace an existing vessel without forcing major field modifications to piping or foundations.
The selected compression concept is a water-injected oil-free rotary screw compressor selected for clean air service with variable industrial demand. The reference package is rated at approximately 11.0 m3/min free-air delivery with a nominal drive rating of about 90 kW at 9.0 bar(g). Its control philosophy is variable-speed or modulating control depending on package design. This arrangement is appropriate because the application shows strong pulsed demand at each blow cycle with very high instantaneous flow relative to average consumption. The compressor is sized first for the sustained process demand, while the receiver is used to bridge short-duration deviations and provide control stability. That separation of roles avoids the common mistake of oversizing compressor capacity merely to satisfy a peak that lasts only a few seconds.
A key advantage of this compressor concept is oil-free compression with a compact rotary architecture. The receiver supports that behavior by slowing pressure changes at the control point. With fixed-speed or staged machines, useful storage can lengthen loaded and unloaded intervals and reduce rapid cycling. With variable-speed machines, storage allows the drive time to accelerate or decelerate instead of chasing every small transient. With multi-compressor stations, the receiver can prevent a short demand pulse from unnecessarily starting a larger trim or standby machine. The final control logic still belongs to the compressor package and system controller; the receiver does not replace correct sequencing. Its role is to create a pressure buffer that gives the control system time to make stable decisions.
The principal system parameters are 11.0 m3/min FAD, approximately 90 kW installed compressor power and 9.0 bar(g) compressor discharge pressure. The useful header is planned near 8.5 bar(g), leaving roughly 0.5 bar for treatment and distribution losses under the reference condition. The average demand estimate of 7.8 m3/min represents about 71% of rated FAD, which leaves approximately 29% nominal capacity between average demand and compressor rating. This margin is not automatically spare capacity for future expansion; it also covers normal production variability, treatment purge losses where applicable, and uncertainty in the initial demand estimate.
The selected high-pressure dryer or appropriately rated downstream treatment package and filtration train must be rated for the actual inlet conditions and peak flow. Pressure drop through the treatment package should be checked when elements are clean and again at the maximum acceptable differential pressure, because a receiver cannot compensate for a chronically undersized filter or dryer. Instrumentation should include compressor discharge pressure, receiver pressure and downstream header pressure so that commissioning personnel can distinguish a storage problem from a piping or treatment restriction. Where the process is sensitive to moisture, pressure dew point should be measured downstream of the dryer rather than inferred from compressor-room temperature. These details make the case representative of a complete compressed-air system instead of a tank-only equipment description.
The demand profile is characterized by strong pulsed demand at each blow cycle with very high instantaneous flow relative to average consumption. During a fast load increase, the compressor controller sees pressure begin to fall and commands more capacity. The receiver supplies part of the temporary deficit while the machine accelerates, loads another stage or brings a second compressor online. During a fast load decrease, the process reverses: excess compressor delivery enters the receiver and the rate of pressure rise is reduced. The magnitude of this benefit depends on the usable pressure band.
The full geometric volume of 2,500 L is not 'available air' at atmospheric conditions; only the mass released between the upper and lower useful pressures can support the process. The reference control philosophy therefore links receiver sizing to actual set points. If the plant narrows its pressure band without changing storage, the seconds of useful buffer become shorter. If it raises the upper pressure simply to create more storage, energy consumption and pressure-vessel requirements can increase. A better approach is to define the true minimum user pressure, minimize avoidable distribution loss and then size storage around the allowable pressure swing. For this case, the 2.5 m3 vessel acts as a system buffer rather than an emergency air reservoir. Any safety-critical pneumatic reserve - for example a valve that must complete a fail-safe stroke after compressor loss - would be calculated separately and may require a protected dedicated receiver with check valves and its own pressure band.
The reference receiver capacity is 2,500 L. That selection is plausible for a compressor delivering 11.0 m3/min FAD, but the reasoning is not a fixed liters-per-kilowatt rule. Receiver volume depends on compressor control type, acceptable cycling frequency, peak-event duration, upper and lower pressures, and whether the storage is centralized or located close to a high-demand user. In this application, the vessel is intended to smooth the main system and absorb the short peaks described above. If field logging later shows that one remote machine causes most of the pressure disturbance, a smaller point-of-use receiver near that machine could be more effective than increasing central storage.
For engineering review, the team should calculate usable stored mass between the normal upper pressure and the minimum acceptable process pressure, then compare that air quantity with the deficit between peak demand and compressor supply over the event duration. The calculation should also account for the compressor continuing to deliver air while the receiver is discharging. The 2,500 L selection is therefore a coordinated starting point, not an isolated catalog choice. It provides enough volume to demonstrate stable control behavior while remaining compatible with the available footprint and the selected vertical geometry. If future production adds significant load, the original receiver can remain useful as base storage while additional distributed storage or compressor capacity is added through planned branch connections.
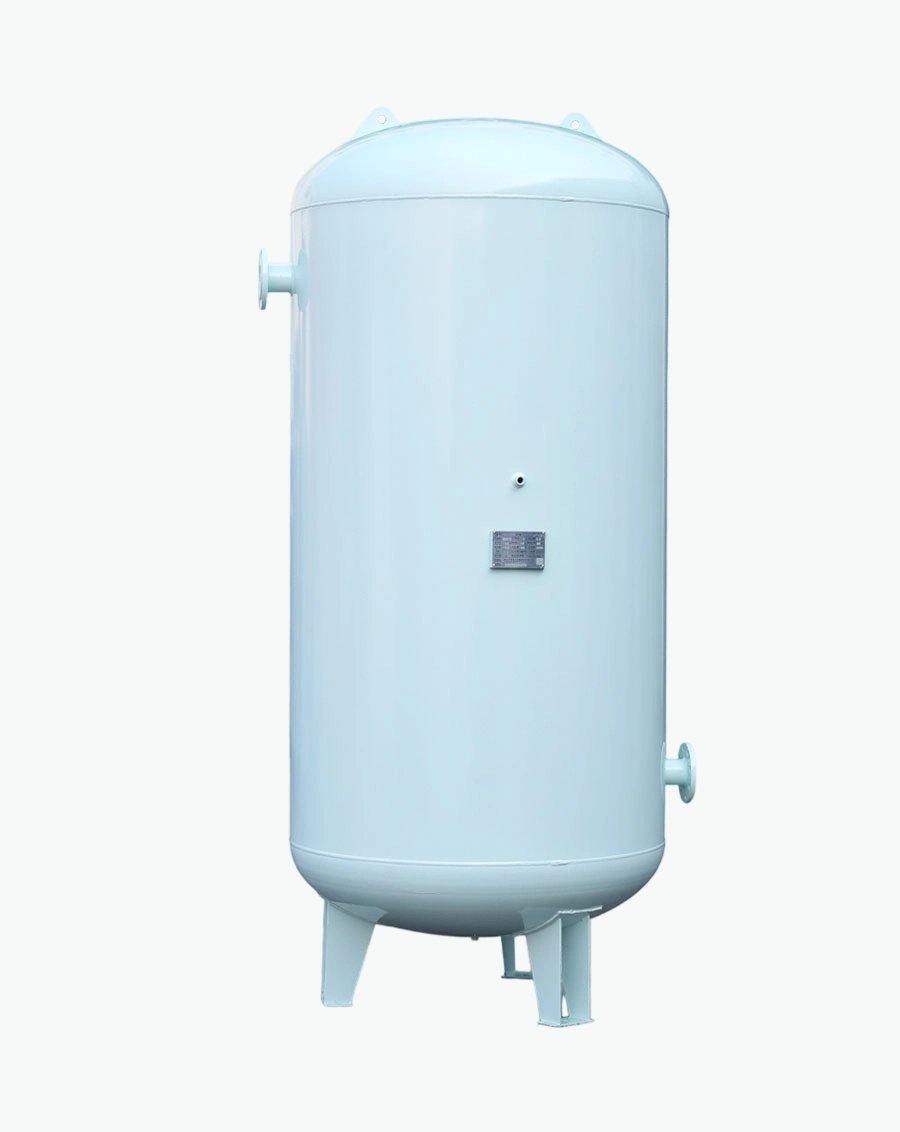
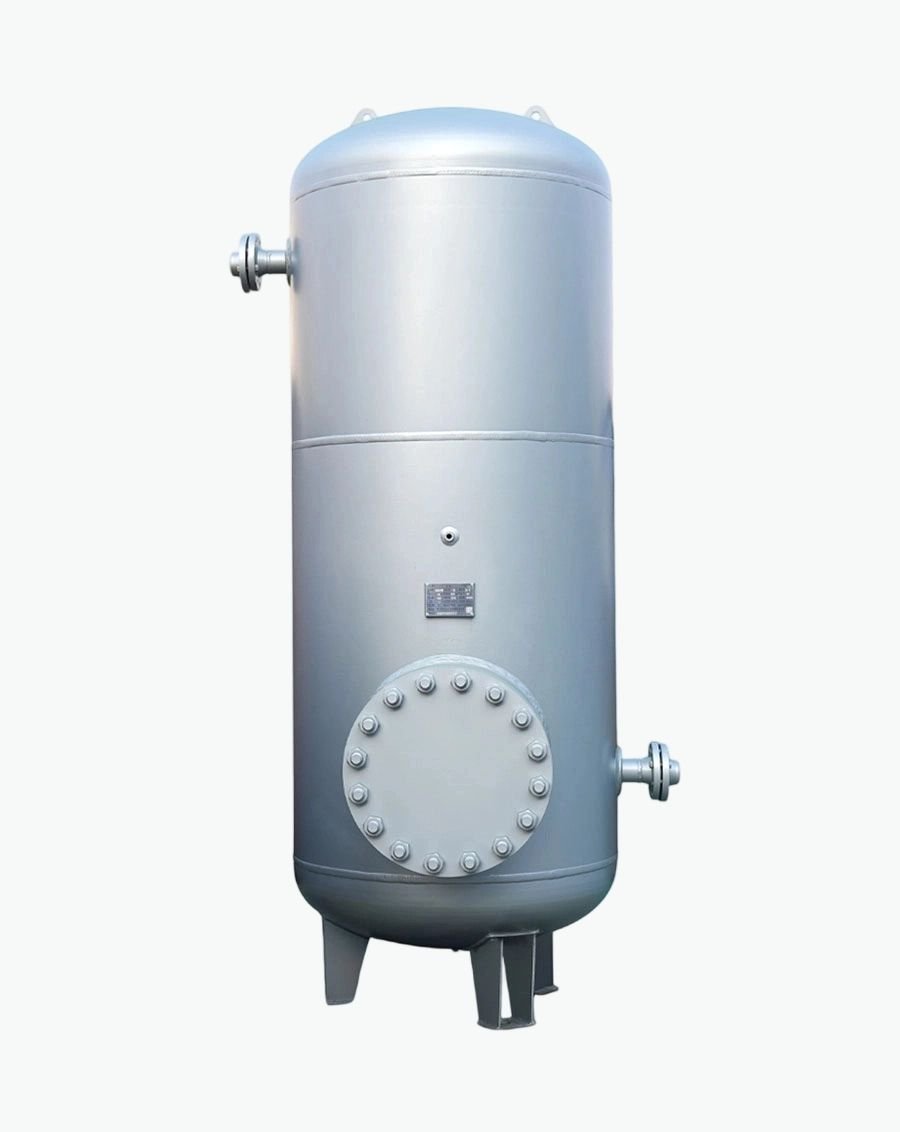
A vertical receiver was chosen with a nominal diameter of 1,200 mm and an overall reference height of about 3,010 mm. The orientation reflects site integration rather than pressure performance alone. Vertical vessels normally save floor area and can simplify low-point drainage, but they require adequate overhead clearance, foundation stability and access to upper nozzles. Horizontal vessels reduce overall elevation and can fit under pipe racks or mezzanines, but they use more floor length and require saddle support at two locations. In either case, nozzle orientation is reviewed against the actual compressor skid, dryer, header and maintenance aisles before the fabrication drawing is released.
The estimated empty vessel weight is about 1,350 kg, so lifting points and foundations must be designed around the real center of gravity and any attached valves or piping. Shipping geometry also matters. A vessel that fits the plant may still require detachable instruments, protected nozzles or special transport supports to move through a container, truck route or plant doorway. The custom-manufacturing process therefore coordinates diameter, support spacing, lifting lugs, access openings and nozzle projection rather than optimizing only the internal volume. This integration work can reduce field welding and allows the customer to plan concrete pads, anchor bolts and pipe-support locations before the vessel arrives.
The reference tank material is 304L stainless steel. Material selection is tied to service conditions, not simply to the application name. Carbon steel is widely suitable for general compressed-air service when condensate is controlled, corrosion allowance and coating are correctly specified, and the receiver can be drained. Stainless steel can be justified where wet service, washdown, clean-utility expectations or corrosion risk make carbon steel less attractive. The receiver in this case is intended for oil-free dry compressed air. The project team would still confirm the exact material specification, impact-test requirement if any, allowable stress, corrosion allowance and compatibility with the governing pressure-vessel code before purchase of plate and fittings. Internal corrosion risk changes with receiver position.
A wet receiver immediately after the compressor sees warm saturated air and usually collects more condensate, while a dry receiver after a correctly performing dryer sees much less liquid water. The external environment is also relevant because the site includes high-speed packaging halls where high-pressure piping and safety segregation require careful layout. Carbon-steel vessels therefore need a coating system matched to exposure and surface preparation. Stainless-steel vessels need controlled fabrication practices that prevent carbon-steel contamination and may require pickling or passivation depending on the specification. These choices are part of pressure-vessel engineering and manufacturing quality; they should be decided before fabrication rather than treated as cosmetic finishing after the tank is complete.
The preliminary inlet connection is 1-1/2-inch BSP(F) threaded and the outlet is DN50 PN16 flanged. These sizes are selected from the reference compressor flow and pressure so gas velocity and pressure drop remain reasonable. They are not chosen from receiver volume alone. At 9.0 bar(g), the actual volumetric flow inside the pressurized pipe is far lower than the stated FAD at atmospheric reference conditions, which is why connection sizing should be based on the compressed-state flow, allowable velocity, fitting losses and the length of the surrounding piping. For a large flow system, one nominal size increase can materially reduce pressure drop and improve how quickly the stored volume can respond to a transient.
The nozzle schedule must also consider field alignment. Inlet and outlet centerlines are coordinated with the compressor discharge, treatment package and main header to minimize unnecessary elbows and stressed field connections. The safety valve connection is preliminarily DN32 PN16 flanged; final valve capacity and orifice selection must be determined by the applicable relief-sizing rules and the maximum credible inflow. The drain is dn15 threaded drain connection for automatic or manual drain, and the pressure gauge uses a g1/2 bsp(f) pressure-gauge connection. Isolation valves should permit maintenance without trapping an unsafe unprotected volume. Where a check valve is used, its effect on receiver charging and discharging must be understood so the tank remains connected to the pressure zone it is intended to stabilize.
The receiver may be installed before or after the high-pressure dryer or appropriately rated downstream treatment package, and that location changes its operating duty. A wet receiver placed upstream of the dryer can provide cooling time, reduce velocity and collect bulk condensate before air enters treatment equipment. This can reduce short-term flow fluctuations at the dryer inlet, but the vessel experiences the highest moisture load and therefore needs reliable automatic drainage.
A dry receiver downstream of treatment stores conditioned air and can support sensitive users without forcing the dryer to follow every short peak. Some installations use both wet and dry storage when pressure stability and air quality are both critical. For this case, drainage is treated as a functional design item. A blocked or undersized drain reduces effective storage as water accumulates and increases corrosion risk in carbon-steel service. The low-point connection has to remain accessible after the vessel is installed, and the drain should discharge to an appropriate condensate-management system rather than directly to the floor. If the receiver is outside or in a cold area, drain lines require freeze protection. If the plant uses oil-injected compressors, condensate disposal should account for oil content. Where the application requires oil-free air, the receiver itself must be cleaned and protected so fabrication residues do not compromise the treatment strategy.
The working pressure for the application is 9.0 bar(g), but formal vessel design requires a separate design pressure and design temperature that include the applicable operating margin and code rules. The nominal shell thickness shown for this case is 10 mm. That value is a preliminary engineering reference only. Final required thickness must be calculated using the selected material allowable stress, weld-joint efficiency, inside diameter, design pressure, corrosion allowance and any code-specific minimums. Formed-head thinning, nozzle reinforcement, external loads, vacuum conditions if relevant, cyclic service and transport loads also have to be considered before the drawing becomes a manufacturing document.
The receiver must be protected against overpressure by a correctly selected pressure-relief device, and the relief path must not be isolated during operation. The safety valve connection stated in the parameter table is only the vessel nozzle provision; it does not constitute a relief-capacity calculation. Pressure gauges should be readable from the normal operating position and selected with an appropriate range. The manufacturer should apply the pressure test, nondestructive examination, documentation and marking required by the governing jurisdiction. For international supply, code and registration requirements can differ by destination, so the technical and commercial review should establish them before material procurement. This approach prevents a website case study from implying certification that has not been defined for a real order.
For a specialist air-receiver manufacturer, customization starts before steel is cut. Engineering personnel review compressor flow, operating pressure, control band, receiver role, preferred orientation, nozzle elevations, connection standards, drainage strategy, support arrangement and installation restrictions. A general arrangement is then developed around the 2,500 L nominal volume, 1,200 mm diameter and vertical configuration. The goal is not to make every vessel unique for its own sake; it is to change only the features that improve fit, reliability, code compliance or installation efficiency.
This can include nozzle orientation, flange standard, drain location, support dimensions, lifting points, coating and instrument connections. The reference project also illustrates why coordination with compressor OEMs, distributors and system integrators is valuable. Those partners often know the package interface and site piping before the final vessel design begins. By exchanging dimensional drawings and line lists early, the receiver can arrive with connections that align to the skid rather than requiring field adapters. For replacement projects, existing foundation dimensions and nozzle coordinates can be incorporated where code and design constraints allow. For new systems, the vessel drawing can be released early enough for civil and piping teams to plan around the real equipment envelope. This engineering support is a meaningful part of custom manufacturing because it reduces uncertainty outside the vessel shop.
Manufacturing begins with controlled material identification and traceability. Plate, heads, pipe and flanges are checked against the approved bill of materials and the specified pressure-vessel standard. Formed components are inspected for dimensions and minimum thickness before assembly. Welding is performed using qualified procedures and qualified personnel appropriate to the material and code. Joint preparation, fit-up and weld sequencing are controlled to maintain alignment and reduce distortion, especially around nozzles and supports where local stresses can be introduced by poor fabrication practice. Inspection requirements depend on the code, material, thickness and service.
They can include visual examination, dimensional inspection, radiography, ultrasonic examination, magnetic-particle or liquid-penetrant testing as specified by the design and quality plan. No single nondestructive examination statement should be copied across every international project without checking the applicable rules. After required examination is accepted, the vessel undergoes the code-defined pressure test and a final dimensional review. Surface treatment, painting, passivation or other finishing is completed according to the approved specification. The delivery dossier should match the vessel actually manufactured, including material records and inspection reports rather than generic marketing certificates.
Before installation, the site team checks the vessel nameplate or data sheet, lifting plan, foundation, anchor locations and pipe support. The receiver should not be used to carry unplanned piping loads; connected lines need independent support and enough flexibility to avoid transferring thermal movement or misalignment into the nozzles. The vertical layout must provide access to the drain at the low point, the pressure gauge, the relief device and isolation valves. The safety valve discharge should be routed or guarded as required by the site. Any shipping braces or protective caps are removed only when the vessel is ready for final connection. Commissioning then verifies valve position, drain function, instrument range, leak tightness and correct operation of the compressor control system. The air network is pressurized gradually while receiver and header pressures are observed.
A useful acceptance check is to compare pressure response during known production events before and after the receiver is placed in service. If the header still falls rapidly, the team should investigate branch restrictions, pressure-regulator settings, dryer or filter differential pressure and compressor-control delays rather than assuming the tank is undersized. The final objective is a stable integrated system. The receiver succeeds only when its stored volume can move freely to the users and control sensors that depend on it.
Compressed-air energy performance is affected by both pressure level and control stability. Operating at a higher pressure than the process requires increases compressor work and can increase artificial demand at unregulated users. The receiver supports energy control by allowing the compressor system to operate within a practical pressure band instead of responding to every second-by-second fluctuation. For water-injected oil-free rotary screw service, this helps the selected control method remain stable and reduces unnecessary transitions. The receiver does not create energy savings by itself; savings occur when storage, pressure control and compressor sequencing are designed together.
Reliability planning includes periodic inspection of the vessel, safety valve, pressure gauge, drain and isolation valves according to the jurisdiction and plant maintenance program. Automatic drains should be function-tested because a silent drain failure can gradually fill the vessel with condensate and reduce effective storage. Coatings are inspected for damage, and stainless-steel surfaces are protected from contamination or aggressive cleaners that are not compatible with the grade. Pressure trends can be logged over time to detect increasing filter differential pressure or changes in plant demand. These maintenance practices preserve the receiver's operating value and provide data for future expansion decisions.
The case is sized around current demand plus a practical operating margin, not an assumption of unlimited future growth. Oversizing every compressor and receiver increases capital cost, floor-space use and sometimes inefficient unloaded operation, while undersizing can create unstable pressure and excessive cycling. A modular approach is therefore preferred. The piping layout can reserve a branch for future storage, the main header can be checked for the expected next-stage flow, and multi-compressor controls can be selected with expansion in mind. The existing 2,500 L receiver can remain part of the final system even if an additional compressor or local receiver is installed later.
For the customer, the value of a custom receiver manufacturer is the ability to translate compressed-air system requirements into a pressure vessel that fits the real package. That includes matching 9.0 bar(g) service pressure, 11.0 m3/min compressor flow, 2,500 L storage, 304L stainless steel, nozzle standards and a vertical site envelope. The manufacturer must also recognize the limits of preliminary website data. Final design requires confirmed process conditions, applicable code, formal calculations and approved drawings. By making those boundaries clear while still explaining the engineering logic, this case demonstrates professional support for compressor OEMs, distributors, EPC contractors, system integrators and end users without presenting an illustrative configuration as an undocumented completed customer order.
Consider a short production event in which demand rises from the approximate average of 7.8 m3/min toward 13.8 m3/min. The compressor can provide about 11.0 m3/min at its rated condition, so the difference between peak demand and current compressor output is supplied temporarily by stored air while the control system reacts. The receiver pressure begins to fall, but the aim is to keep the downstream header above the minimum required by the process. Once the compressor reaches the commanded capacity or an additional machine starts, the deficit closes and the receiver can recharge. This is the normal dynamic function of storage; it is not an indication that the compressor is undersized if the peak is brief and planned.
Now consider the opposite event: several users stop at once. Compressor delivery briefly exceeds demand, and the receiver accepts the difference. Pressure rises more slowly, giving the controller time to unload, slow down or sequence a machine off. A receiver that is too small would allow a rapid pressure swing and more frequent control transitions. A receiver that is excessively large could slow recovery and occupy unnecessary space. The 2,500 L selection is intended to provide a balanced response for the reference demand pattern. Field data would refine this balance by showing the real duration and frequency of both rising and falling demand events.
Pressure-control quality also depends on where the system is measured. If the compressor transducer is installed at the package discharge while the receiver and major pressure losses are farther downstream, the controller may not see the pressure experienced by production equipment. If the transducer is too far away, signal delay and network dynamics can also make control unstable. The reference arrangement uses pressure measurement points at compressor discharge, receiver and production header so commissioning staff can separate compressor behavior from treatment and distribution losses. Data logging during representative production is especially useful when the plant has strong pulsed demand at each blow cycle with very high instantaneous flow relative to average consumption.
The receiver itself may include a local gauge for safe operation and maintenance, while electronic sensors for sequencing are installed in the common header. Sensor isolation valves should be arranged so maintenance does not leave the system without overpressure protection or control feedback. The pressure gauge connection shown in the parameter table is therefore only one part of the instrumentation concept. A professional system integrator will also define alarm set points, low-pressure warnings and controller response to a failed sensor. These details help the stored air support a predictable control system rather than act as an uncontrolled volume attached to the network.
Parameter Name | Reference Value |
Horizontal / Vertical | Vertical |
Weight | 1,350 kg (preliminary empty weight) |
Diameter | 1,200 mm |
Height | 3,010 mm overall reference height |
Wall Thickness | 10 mm nominal shell thickness - preliminary only |
Tank Material | 304L stainless steel |
Suitable Medium | Oil-free dry compressed air |
Capacity | 2,500 L |
Ambient Temperature | -10 to +45 C |
Working Pressure | 9.0 bar(g) |
Inlet Port Size | 1-1/2-inch BSP(F) threaded |
Outlet Port Size | DN50 PN16 flanged |
Safety Valve Connection | DN32 PN16 flanged connection; final valve/orifice to be sized by code |
Drain Valve Connection | DN15 threaded drain connection for automatic or manual drain |
Pressure Gauge Connection | G1/2 BSP(F) pressure-gauge connection |
Engineering use note: the 15 values above are internally coordinated with the reference compressor system and are intended to demonstrate how a custom receiver can be selected around flow, pressure, control behavior, installation space and air quality. Nominal shell thickness, weight, nozzle sizes and relief connection are preliminary values only. Final design must confirm design pressure and temperature, material specification, corrosion allowance, joint efficiency, head thickness, nozzle reinforcement, supports, external loads, test pressure, relief capacity and all jurisdictional requirements before fabrication.
Specializing in pressure vessel manufacturing, we provide reliable, certified, and customized solutions for customers across diverse industries worldwide.
No.268 Xinda Road, High-tech Industrial Park, Longkou City,Shandong Province
Copyright © 2026 Yantai Xinglong Pressure Vessel Manufacturing Co., Ltd All Rights Reserved.


 عربي
 Español
 Русский
