Stay updated with the latest company news, product innovations, exhibition highlights, and industry trends. Explore valuable insights into pressure vessel technologies and global markets.
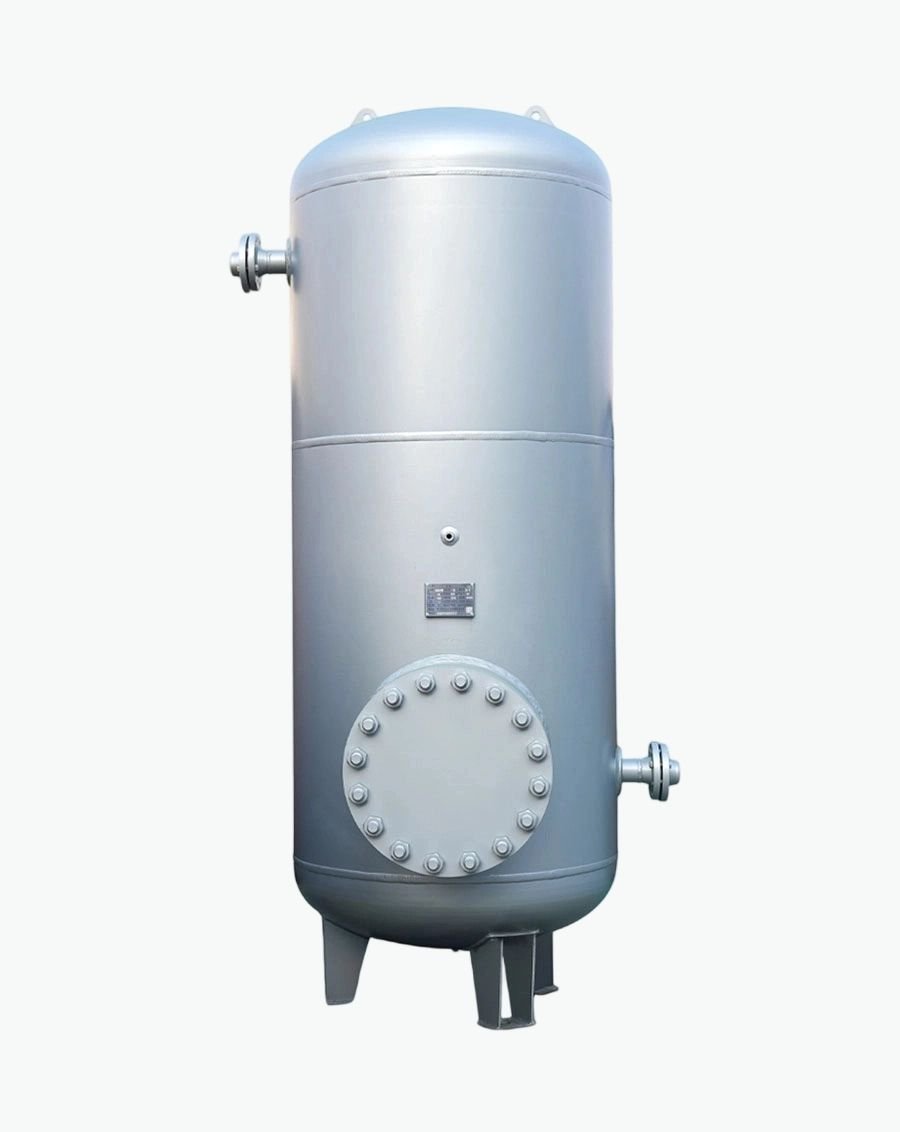
Compressed air systems represent one of the most energy-intensive utility services in industrial facilities, typically consuming 10-30% of total electrical power in manufacturing operations. Within these systems, air receiver tanks play a disproportionately important role in overall energy efficiency that extends far beyond their simple function as compressed air storage vessels. Properly sized, strategically located, and effectively managed receiver tanks enable significant energy savings through compressor load optimization, pressure stabilization, condensate management, and system control enhancement.
Despite their critical importance, air receivers frequently receive inadequate attention during system design, often being undersized, poorly positioned, or operated without understanding their impact on energy consumption. This oversight results in unnecessary compressor cycling, excessive pressure drops, increased maintenance costs, and premature equipment failures that compound operational expenses throughout the system lifecycle.
This comprehensive analysis examines the multifaceted contributions of air receiver tanks to compressed air energy efficiency, providing engineering professionals, facility managers, and energy auditors with actionable insights for optimizing receiver tank applications. By understanding the thermodynamic principles, control strategies, and operational practices governing receiver performance, organizations can unlock substantial energy savings while improving system reliability and extending equipment service life.
Air receiver tanks store energy in the form of pressurized air, with stored energy content directly proportional to both volume and absolute pressure according to ideal gas law relationships. The theoretical energy stored in a receiver tank equals the work required to compress atmospheric air to storage pressure, expressed mathematically as: E = (P × V) / (k - 1) × [1 - (P_atm / P)^(k-1)/k]
Where E represents stored energy (Joules), P is absolute pressure (Pa), V is volume (m³), P_atm is atmospheric pressure, and k is the specific heat ratio (1.4 for air). This relationship demonstrates that doubling receiver volume doubles stored energy capacity, while increasing pressure yields diminishing returns due to the exponential term.
Practical implications guide sizing decisions: larger volumes provide greater energy buffering capacity enabling longer compressor off-times during low demand periods. However, physical space constraints, structural support requirements, and cost considerations establish practical upper limits on receiver sizing. Optimal designs balance energy storage benefits against installation feasibility and capital investment.
Temperature effects significantly influence stored energy calculations. Compression processes generate heat raising air temperature well above ambient conditions (often 80-150°C at compressor discharge). As compressed air cools within the receiver, pressure decreases following Gay-Lussac's law (P/T = constant at constant volume). This cooling effect releases thermal energy to surroundings while reducing usable pressure, representing an inherent energy loss mechanism unless heat recovery systems capture waste thermal energy.
Moisture condensation during cooling further impacts energy storage efficiency. Water vapor present in compressed air condenses as temperature drops below dew point, releasing latent heat but reducing gas volume available for pressure maintenance. The condensed liquid occupies minimal volume compared to vapor phase but requires regular drainage to prevent accumulation compromising effective storage capacity.
Theoretical compression processes fall along a spectrum between isothermal (constant temperature) and adiabatic (no heat transfer) extremes. Real-world compressors operate somewhere between these ideals depending on design, cooling effectiveness, and compression speed. Isothermal compression requires less work input than adiabatic processes because continuous heat removal prevents temperature rise increasing resistance to further compression.
Receiver tanks contribute to approaching isothermal behavior by providing residence time for heat dissipation. Large surface area-to-volume ratios enhance cooling rates, though practical receivers prioritize volume over surface area for economic reasons. External fins, forced air circulation, or water jacketing improve heat transfer but add complexity and cost rarely justified for standard industrial applications.
Multi-stage compression systems with intercoolers between stages approximate isothermal compression more closely than single-stage designs. Receiver tanks positioned after final compression stages benefit from reduced inlet temperatures, improving storage density and reducing thermal stress on vessel materials. Understanding these thermodynamic interactions enables optimized system configurations maximizing energy efficiency.
Compressor short-cycling—frequent starts and stops occurring multiple times perminute—represents one of the most damaging and energy-wasteful operating modes. Each start cycle draws high inrush current (5-7 times running current) stressing electrical components, mechanical linkages, and lubrication systems. Motor windings experience thermal cycling accelerating insulation degradation, while crankshaft bearings endure loads reducing service life.
Energy penalties from short-cycling include:
● Inrush current losses consuming 20-40% more energy than steady-state operation during acceleration
● Unloaded running periods where compressors consume 30-60% of full-load power without producing useful compressed air
● Reduced volumetric efficiency during transient startup before reaching optimal operating conditions
● Increased maintenance frequency for starters, contactors, belts, and couplings subjected to cyclic stresses
Adequately sized receiver tanks eliminate short-cycling by providing sufficient storage volume to satisfy demand fluctuations between compressor cycles. General guidelines recommend receiver capacity of 1 gallon per CFM of compressor output for fixed-speed units, or 2-4 gallons per CFM for variable speed drives requiring additional buffering. These rules-of-thumb translate to approximately 7-30 liters per m³/min depending on control strategy.
Proper receiver sizing enables compressors to operate in stable loaded/unloaded cycles with minimum run times of 5-10 minutes and off-times of 2-5 minutes, dramatically reducing start-stop frequency. Advanced control systems monitor receiver pressure trends predicting demand patterns and adjusting compressor sequencing to minimize transitions while maintaining adequate supply pressure.
Different compressor types employ distinct control methodologies benefiting differently from receiver tank integration:
Fixed-Speed Load/Unload Controls: These simplest controls switch compressors between fully loaded (producing air) and unloaded (spinning without compression) states based on pressure switches. Receivers absorb demand spikes during unloaded periods preventing pressure drops triggering unnecessary additional compressor starts. Larger receivers extend unload times improving part-load efficiency since unloaded operation still consumes significant power.
Variable Speed Drives (VSD): VSD compressors modulate motor speed matching output to demand, theoretically eliminating cycling. However, VSDs exhibit reduced efficiency at low speeds (<40% capacity) and require minimum run times preventing rapid modulation.
Receivers buffer short-term demand variations allowing VSDs to operate at optimal speeds rather than constantly adjusting to transient fluctuations. Combined VSD-receiver systems achieve superior part-load efficiency compared to either technology alone.
Multi-Compressor Sequencing: Facilities with multiple compressors benefit from centralized controllers coordinating unit operation based on system demand. Receivers provide the hydraulic capacitance enabling smooth transitions between compressors entering or leaving service. Without adequate storage, pressure transients during sequencing create instability causing hunting behavior where compressors repeatedly start and stop fighting each other's output.
Start/Stop Controls: Small compressors (<10 HP) often use simple pressure switches turning motors completely off when pressure reaches cut-out setpoint. These systems critically
depend on receiver capacity to limit cycling frequency. Undersized receivers cause excessive cycling damaging motors and controls while wasting energy through repeated inrush
currents.
Compressor control systems maintain system pressure within defined bands (e.g., 7-8 bar, 100-115 psi). Wider pressure bands allow longer compressor run times and off periods
improving efficiency but require larger receivers to prevent pressure dropping below minimum during off cycles. Narrower bands maintain tighter pressure control but force more frequent cycling demanding precise receiver sizing.
Optimal pressure band selection balances energy efficiency against application pressure requirements. Every 1 bar (14.5 psi) increase in system pressure raises compressor energy consumption by approximately 7% due to increased compression work. Therefore, operating at the lowest acceptable pressure maximizes efficiency. Receivers enable lower average system pressures by absorbing demand spikes that would otherwise cause pressure dips requiring higher baseline pressures as safety margin.
Smart pressure control systems continuously adjust setpoints based on real-time demand patterns, gradually lowering pressures during low-demand periods while maintaining adequate margins for peak requirements. This dynamic optimization requires sufficient receiver capacity to prevent rapid pressure excursions triggering compressor responses before control algorithms can react.
Pressure Stabilization and Demand Smoothing Attenuating Demand Fluctuations Industrial compressed air demand exhibits considerable variability driven by production schedules, batch processes, tool usage patterns, and operational changes. Peak demands may exceed average consumption by factors of 2-5x for brief periods, while nighttime or weekend operations may drop to 10-20% of peak levels. These fluctuations challenge compressor response capabilities and create pressure instability without adequate buffering.
Receiver tanks function as hydraulic capacitors smoothing demand profiles presented to compressors. When sudden high-flow events occur (pneumatic cylinder actuation, sandblasting operations, large valve openings), receivers supply immediate flow from stored pressure preventing system-wide pressure drops. Compressors respond to the resulting gradual pressure decline at manageable rates rather than reacting to instantaneous demand spikes.
Quantitative analysis demonstrates receiver effectiveness using the formula: ΔP = (Q_demand - Q_supply) × Δt / V_receiver
Where ΔP represents pressure change, Q_demand and Q_supply are volumetric flow rates, Δt is time duration, and V_receiver is receiver volume. This relationship shows that doubling receiver volume halves pressure change rate for identical demand-supply imbalances, providing operators with predictable pressure stability characteristics.
Applications with highly intermittent demand patterns particularly benefit from receiver buffering. Examples include:
● Packaging machines with cyclical pneumatic actuator sequences
● Automotive assembly lines with spot welding and riveting operations
● Woodworking shops with occasional high-flow sanding or spraying
● Textile mills with periodic loom operations creating pulsed demand
In these scenarios, properly sized receivers enable smaller compressor installations by handling peak flows from storage rather than requiring compressors sized for maximum instantaneous demand. Capital cost savings from downsized compressors often offset receiver investment while achieving superior energy efficiency through improved load factors.
Pressure drops throughout distribution systems result from friction losses in piping, fittings, filters, dryers, and flow restrictions. These drops create localized low-pressure zones forcing compressors to maintain higher discharge pressures ensuring minimum pressure reaches distant endpoints. Every bar of unnecessary pressure increase costs approximately 7% additional compressor energy.
Strategically located receiver tanks mitigate pressure drop effects through several mechanisms:
Point-of-Use Receivers: Installing small receivers near high-demand equipment provides local storage compensating for distribution pressure drops. These receivers charge during low-demand periods at system pressure then discharge locally during peak usage, maintaining adequate equipment pressure without elevating entire system pressure. Typical sizes range from 50-500 liters depending on equipment requirements.
Intermediate Boosters: Large facilities with long distribution runs benefit from intermediate receivers positioned at strategic locations dividing the system into pressure zones. These receivers reduce effective pipe length for pressure drop calculations, enabling lower overall system pressures while maintaining endpoint adequacy. Zoned systems also isolate disturbances preventing localized events affecting entire facilities.
Dryer Outlet Receivers: Positioning receivers immediately after air dryers stabilizes pressure entering distribution systems despite dryer pressure fluctuations during regeneration cycles. Desiccant dryers especially exhibit periodic pressure drops during tower switching that receivers absorb preventing downstream pressure instability. Refrigerated dryers show smaller but measurable pressure variations during defrost cycles.
Many pneumatic applications require stable pressure for consistent performance. Pressure fluctuations cause:
● Variable actuator speeds affecting production cycle times and product quality
● Inconsistent spray patterns in painting and coating operations creating finish defects
● Fluctuating clamping forces in machining operations compromising dimensional accuracy
● Unstable instrument readings in process control applications requiring precise pressure references
Receiver tanks dampen pressure oscillations maintaining steady supply conditions enabling consistent application performance. Critical processes may employ dedicated receivers with pressure regulators providing ultra-stable pressure independent of main system variations. While regulators themselves dissipate energy through throttling, the improved product quality and reduced scrap rates often justify the efficiency penalty for sensitive applications.
Compressed air contains significant moisture derived from ambient humidity concentrated by compression ratios. At typical industrial conditions (20°C, 60% RH ambient compressed to 8 bar), every cubic meter of free air delivers approximately 10-15 grams of water vapor. Upon cooling in receivers, much of this vapor condenses forming liquid water requiring removal.
Receivers function as primary moisture separators utilizing gravity settling and velocity reduction. As compressed air enters the receiver, expansion and directional changes reduce velocity allowing water droplets to settle to the bottom. Baffle plates or cyclonic inserts enhance separation efficiency by creating swirling flow patterns throwing droplets outward toward walls where they coalesce and drain downward.
Effective condensate removal requires:
● Adequate residence time (typically 3-5 seconds minimum) for droplet settling
● Proper receiver orientation (vertical preferred for gravity drainage)
● Automatic drain valves removing accumulated liquid before re-entrainment occurs
● Regular maintenance ensuring drains function correctly and don't stick open wasting air
Poor condensate management undermines energy efficiency through multiple pathways:
● Accumulated water reduces effective storage volume decreasing buffering capacity
● Liquid carryover damages downstream equipment (dryers, filters, tools) increasing maintenance costs
● Water in pneumatic tools reduces efficiency and accelerates wear requiring premature replacement
● Corrosion from standing water weakens receiver walls potentially causing leaks wasting compressed air
Compression processes convert electrical energy primarily into heat (approximately 90% of input power), with only 10-15% remaining as useful compressed air energy. This waste heat represents a significant recovery opportunity offsetting facility heating costs or preheating process streams.
Receiver tanks participate in heat recovery systems through:
● Direct Heat Exchange: Large receiver surface areas radiate heat to surrounding spaces providing incidental space heating in winter months. Forced air circulation over receiver surfaces enhances heat transfer rates for dedicated recovery systems.
● Water Jacket Integration: Some receivers incorporate water jackets circulating facility
water or glycol solutions capturing heat for domestic hot water, space heating, or process preheating. These systems require careful design preventing thermal stress from
temperature gradients.
● Thermal Storage: Receivers storing hot compressed air effectively function as thermal
batteries, releasing heat gradually as air cools. This passive recovery requires no additional equipment though capture efficiency remains limited compared to active systems.
Quantifying heat recovery potential helps justify receiver sizing investments. A 100 kW
compressor generates approximately 90 kW of waste heat. Capturing even 30-40% through receiver-integrated systems offsets substantial heating fuel costs, improving overall system energy balance beyond compressed air efficiency metrics alone.
Modern compressed air controllers utilize sophisticated algorithms optimizing multi-compressor operations based on real-time demand forecasting, energy pricing signals, and equipment health monitoring. These systems require adequate receiver capacity providing the time constants necessary for predictive control strategies.
Specific control enhancements enabled by proper receiver sizing include:
Demand Forecasting: Controllers analyze historical demand patterns predicting future requirements and pre-positioning compressor capacity accordingly. Receivers provide the temporal buffer allowing compressors to ramp up gradually before predicted demand peaks rather than reacting to surprises with emergency starts.
Load Shedding During Peak Pricing: Facilities subject to time-of-use electricity pricing can strategically deplete receiver storage during expensive peak periods while minimizing compressor operation. Off-peak charging rebuilds storage when electricity costs decrease. This arbitrage strategy requires sufficient receiver capacity to bridge peak pricing windows without compromising production.
Predictive Maintenance Integration: Monitoring receiver pressure decay rates during idle periods reveals system leakage levels. Abnormal decay indicates developing leaks requiring investigation before energy waste escalates. Similarly, tracking compressor fill rates identifies performance degradation signaling maintenance needs before catastrophic failures occur.
Energy Dashboard Visualization: Real-time receiver pressure trends displayed on energy dashboards help operators understand system dynamics and identify inefficiencies. Sudden pressure drops reveal unexpected demand events; slow recovery indicates compressor problems or excessive leakage. Visual feedback drives behavioral changes improving operational discipline.
Compressed air leaks represent the largest source of energy waste in most facilities, typically accounting for 20-40% of total compressed air production. Receiver tanks facilitate leak detection through systematic testing procedures:
Shutdown Test: Isolate the receiver from distribution systems during non-production periods and monitor pressure decay rate. Calculate leak volume from pressure drop using ideal gas law relationships. This test quantifies total facility leakage providing baseline metrics for improvement tracking.
Zone Isolation: Install isolation valves dividing distribution systems into zones with individual receivers. Test each zone separately identifying high-leakage areas requiring targeted repair efforts. This approach prioritizes maintenance resources focusing on worst offenders first.
Continuous Monitoring: Permanent pressure sensors on receivers logging data to building automation systems detect abnormal decay patterns indicating new leaks. Automated alerts notify maintenance personnel enabling rapid response before small leaks grow into major energy wasters.
Typical leak costs illustrate the financial impact: a single 3mm hole at 7 bar wastes approximately 2,500 kWh annually costing $250-400 depending on electricity rates. Large facilities may have hundreds of leaks collectively wasting tens of thousands of dollars yearly. Receiver-enabled detection programs pay for themselves quickly through identified savings.
Sizing Methodology
Proper receiver sizing balances energy efficiency benefits against capital costs and space constraints. Recommended approaches include:
Rule-of-Thumb Methods:
● Fixed-speed compressors: 7-10 liters per m³/min (1 gallon per CFM)
● Variable speed drives: 15-30 liters per m³/min (2-4 gallons per CFM)
● Multi-compressor systems: Size for largest single compressor plus 20% margin
These simplified methods provide starting points requiring refinement based on specific application characteristics.
Detailed Calculation Approach:
1 Determine maximum acceptable pressure drop (ΔP_max) during peak demand
2 Calculate peak demand duration (Δt_peak) from historical data or equipment specifications
3 Estimate compressor response delay (Δt_response) including start time and load acceptance
4 Apply formula: V_receiver = (Q_peak × (Δt_peak + Δt_response)) / ΔP_max
This method produces customized sizing matching actual operating conditions rather than generic averages.
Simulation-Based Optimization: Advanced facilities employ compressed air system
simulation software modeling demand profiles, compressor curves, and receiver dynamics. Virtual testing of various receiver sizes identifies optimal configurations balancing energy savings against investment costs. These tools prove valuable for complex multi-compressor systems with variable demand patterns.
Optimal receiver installation maximizes energy efficiency benefits:
Location Selection:
● Place receivers close to compressors minimizing pressure drop in connecting pipes
● Install in climate-controlled spaces preventing freezing in cold environments
● Ensure adequate clearance for maintenance access and future expansion
● Position vertically when possible enhancing condensate drainage
Piping Configuration:
● Use full-size connections matching receiver nozzle diameters avoiding restrictive reducers
● Install isolation valves enabling maintenance without system shutdown
● Include bypass lines around dryers and filters allowing temporary operation during servicing
● Slope connecting pipes toward receivers facilitating condensate return
Instrumentation:
● Install pressure gauges at receiver inlet and outlet monitoring pressure drop across internal components
● Add temperature sensors tracking cooling performance and identifying insulation needs
● Fit automatic drains with failure alarms alerting operators to malfunction before flooding occurs
● Consider flow meters quantifying actual throughput versus compressor capacity utilization
Regular maintenance preserves receiver energy efficiency contributions:
Weekly Tasks:
● Verify automatic drain operation observing discharge during manual test
● Check pressure gauge readings comparing to compressor discharge identifying blockages
● Inspect external surfaces for corrosion, damage, or insulation deterioration
Monthly Tasks:
● Drain receiver manually ensuring complete water removal even if automatic drains appear functional
● Clean strainers or filters in receiver inlet protecting internal surfaces
● Test safety relief valves verifying proper opening pressure and reseating
Annual Tasks:
● Conduct internal inspection during scheduled shutdown checking for corrosion, cracks, or coating deterioration
● Perform hydrostatic testing per regulatory requirements validating structural integrity
● Recalibrate pressure switches and transmitters ensuring accurate control responses
● Update leak detection baselines comparing current decay rates to historical benchmarks
Neglected maintenance gradually degrades receiver performance through accumulated corrosion reducing wall thickness, stuck drains allowing water accumulation, and fouled instruments providing inaccurate control signals. Proactive maintenance programs preserve designed efficiency levels throughout equipment lifecycle.
A mid-sized automotive parts manufacturer operating three 75 kW fixed-speed compressors experienced frequent short-cycling causing excessive maintenance costs and unstable production line pressure. Energy audits revealed compressors cycling 15-20 times hourly with average load factors below 40%.
Solution implementation included:
● Installing 3,000-liter receiver tank (increasing from existing 500 liters)
● Adding point-of-use receivers at three high-demand stamping presses
● Upgrading to automatic electronic drains replacing unreliable float-type units
● Implementing centralized controller coordinating compressor sequencing
Results after six months:
● Compressor cycling reduced to 3-4 times hourly extending equipment life
● Energy consumption decreased 18% (annual savings $24,000)
● Production line pressure stability improved eliminating quality rejects attributed to pressure variation
● Maintenance costs dropped 35% from reduced starter and bearing replacements
● Project payback period: 14 months
A food processing facility with stringent air quality requirements operated five 55 kW oil-free compressors serving packaging, cleaning, and process applications. High energy costs prompted comprehensive system evaluation revealing oversized compressors operating at poor part-load efficiency with inadequate storage buffering.
Interventions implemented:
● Replaced two oldest compressors with single 132 kW VSD unit
● Installed 5,000-liter stainless steel receiver (required for hygiene compliance)
● Added thermal mass receiver integrating with facility hot water system recovering 40 kW waste heat
● Deployed smart controller optimizing compressor operation based on production schedules
Outcomes achieved:
● Total energy consumption reduced 28% despite increased production volume
● Waste heat recovery offset 15% of facility natural gas heating costs
● Air quality improved eliminating moisture-related contamination incidents
● Simplified maintenance from fewer compressors with standardized components
● Carbon footprint reduction of 180 tonnes CO2 annually supporting sustainability goals
Air receiver tanks serve as critical enablers of compressed air system energy efficiency through mechanisms extending far beyond simple air storage. By buffering demand fluctuations, eliminating compressor short-cycling, stabilizing system pressure, facilitating condensate management, and enabling advanced control strategies, properly designed receivers deliver substantial energy savings alongside improved reliability and equipment longevity.
Organizations seeking to optimize compressed air energy efficiency should prioritize receiver assessment and enhancement alongside compressor upgrades and leak repair programs. The relatively modest investment in adequate receiver capacity typically yields attractive returns through reduced energy consumption, lower maintenance costs, improved product quality, and extended equipment service life.
Future developments in smart receiver technologies incorporating IoT sensors, predictive analytics, and integrated heat recovery promise even greater efficiency gains. However,
fundamental principles of proper sizing, strategic placement, and diligent maintenance remain essential regardless of technological sophistication. By applying the insights and best practices outlined in this guide, industrial facilities can unlock hidden energy savings residing within their compressed air receiver infrastructure while building more resilient and sustainable utility systems.
Specializing in pressure vessel manufacturing, we provide reliable, certified, and customized solutions for customers across diverse industries worldwide.
No.268 Xinda Road, High-tech Industrial Park, Longkou City,Shandong Province
Copyright © 2026 Yantai Xinglong Pressure Vessel Manufacturing Co., Ltd All Rights Reserved.


 عربي
 Español
 Русский
